Reducing Detection Time for Sulphate-  Reducing Bacteria in Industrial Water Systems  Les Merrill, CEO, Retego Labs

Reducing Detection Time for Sulphate- Reducing Bacteria in Industrial Water Systems Les Merrill, CEO, Retego Labs

Reducing Detection Time for Sulphate- Reducing Bacteria in Industrial Water Systems
Les Merrill, CEO, Retego Labs

Bacterial contamination does not always lead to material degradation, however, microbiologically influenced corrosion (MIC) continues to present a significant operational and economic challenge across a wide range of industrial sectors, including oil and gas systems, water treatment, and process industries.
A substantial proportion of corrosion-related failures are associated with MIC [1], a complex process in which microbial activity alters localised chemical conditions at metal surfaces, accelerating degradation.

Among the microbial groups implicated in MIC, sulphate-reducing bacteria (SRB) are widely regarded as one of the most significant contributors [2]. These anaerobic microorganisms reduce sulphate to hydrogen sulphide (H2S), a corrosive species that can promote pitting, contribute to sulphide stress cracking, and interfere with corrosion inhibition strategies. The presence of SRB is also associated with oilfield reservoir souring and operational inefficiencies in industrial systems. Despite the well-established role of SRB in corrosion processes, effective monitoring of these organisms remains challenging. Traditional detection methods often involve extended incubation periods or sophisticated laboratory-based analysis, limiting the ability of operators to respond rapidly to changing microbial conditions. As industrial systems increasingly move toward predictive and proactive maintenance strategies, there is a growing need for faster, field-applicable methods of detecting microbial activity.

Limitations of Conventional Detection Techniques

Table 1. Comparison of Conventional and Rapid SRB Detection Methods.
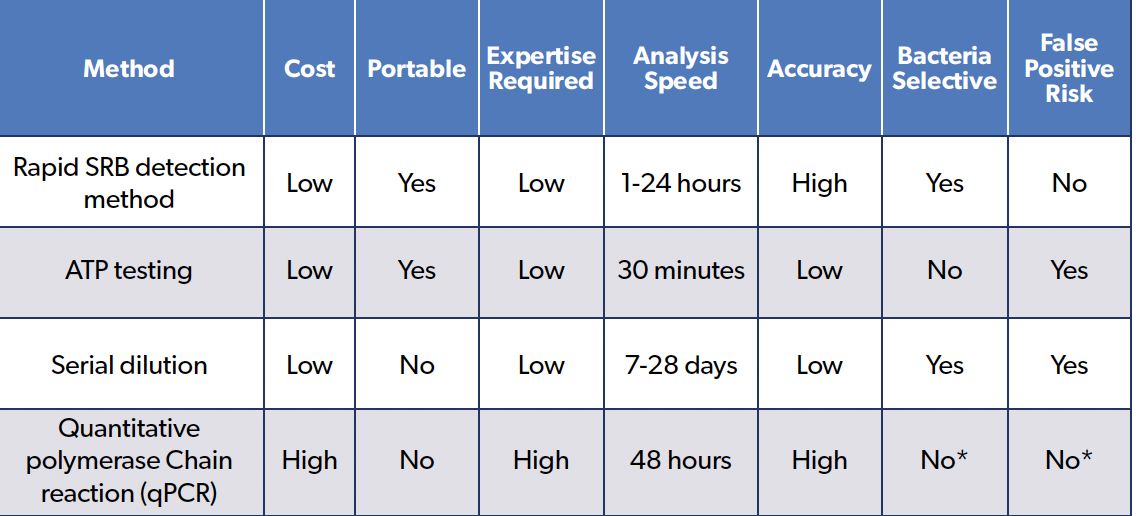
*Note: qPCR selectivity depends on the DNA target primers; however, it cannot distinguish between viable and non-viable microorganisms without propidium monoazide (PMA) sample optimization.

A range of analytical methods has been developed to detect and quantify sulphate-reducing bacteria in industrial water systems. These include culture-based techniques, serial dilution methods, and molecular approaches such as qPCR.

Another commonly used approach utilises adenosine triphosphate (ATP) testing, which measures total microbial activity by quantifying cellular energy present in a sample. While ATP testing provides rapid results and is useful for assessing overall biological activity, it does not distinguish between specific microbial groups such as SRB, limiting its ability to directly assess SRB-related corrosion risk. ATP testing is additionally susceptible to false positives, as it can have difficulty distinguishing between viable and non-viable bacteria [4].

Culture-Based and Serial Dilution Methods

Culture-based methods, including the serial dilution most probable number (MPN) technique, remain widely used due to their relative simplicity, ease of on-site use and historical acceptance [3]. These approaches rely on the growth of microorganisms under controlled conditions to estimate bacterial populations.

However, a key limitation of these methods is the time required to obtain results. Incubation periods may extend up to 28 days before observable changes occur, particularly in samples with low bacterial concentrations. During this time, environmental changes such as oxygen exposure, temperature variation
and sample handling can influence microbial activity and affect accuracy.

In addition, culture-based methods may underestimate microbial populations due to the inability to cultivate all organisms present in a sample, leading to incomplete assessment of microbial activity.

Molecular Techniques

Molecular approaches, including qPCR, offer faster detection compared to culture-based methods and can provide highly sensitive identification of microbial DNA, often within hours to days depending on sample logistics.

Despite these advantages, molecular methods require specialised laboratory infrastructure and trained personnel. Additionally, DNA-based detection does not necessarily indicate active metabolism, as genetic material from non-viable organisms may still be present [5], unless both propidium monoazide (PMA) and photoactivation protocols are optimized for each sample. This limitation can complicate interpretation when assessing current corrosion risk through overestimation of bacterial content.

Operational Implications

The extended timelines and logistical requirements associated with traditional detection methods can delay decision-making in corrosion management. In dynamic industrial environments, a delay of several weeks between sampling and results may result in missed opportunities for early intervention.

Emerging Approaches to Rapid Detection

Alternatives to traditional microbiological detection protocols have led to the development of methods that focus on measuring microbial activity rather than microbial growth. These approaches aim to provide faster and more relevant insights into the presence of metabolically active organisms.

A new method uses two key indicators of SRB activity:

• Enzymatic activity associated with microbial metabolism

• Production of hydrogen sulfide (H2S)

By targeting these indicators, it is possible to detect active SRB populations without prolonged incubation.

Case Example: Rapid Detection of SRB Activity

A field-deployable detection approach has been recently developed and evaluated that combines biological and chemical indicators to assess the presence of sulphate-reducing bacteria in water samples. The method employs two complementary detection pathways:

• Biological detection: Enzymatic activity from SRB produces a fluorescent signal through reaction with a substrate.

• Chemical detection: Hydrogen sulfide (H2S) from the sample reacts with a reagent to generate a visible color change.

These combined mechanisms allow for detection of active SRB without requiring propagation of the organism.

Rapid SRB Detection Workflow
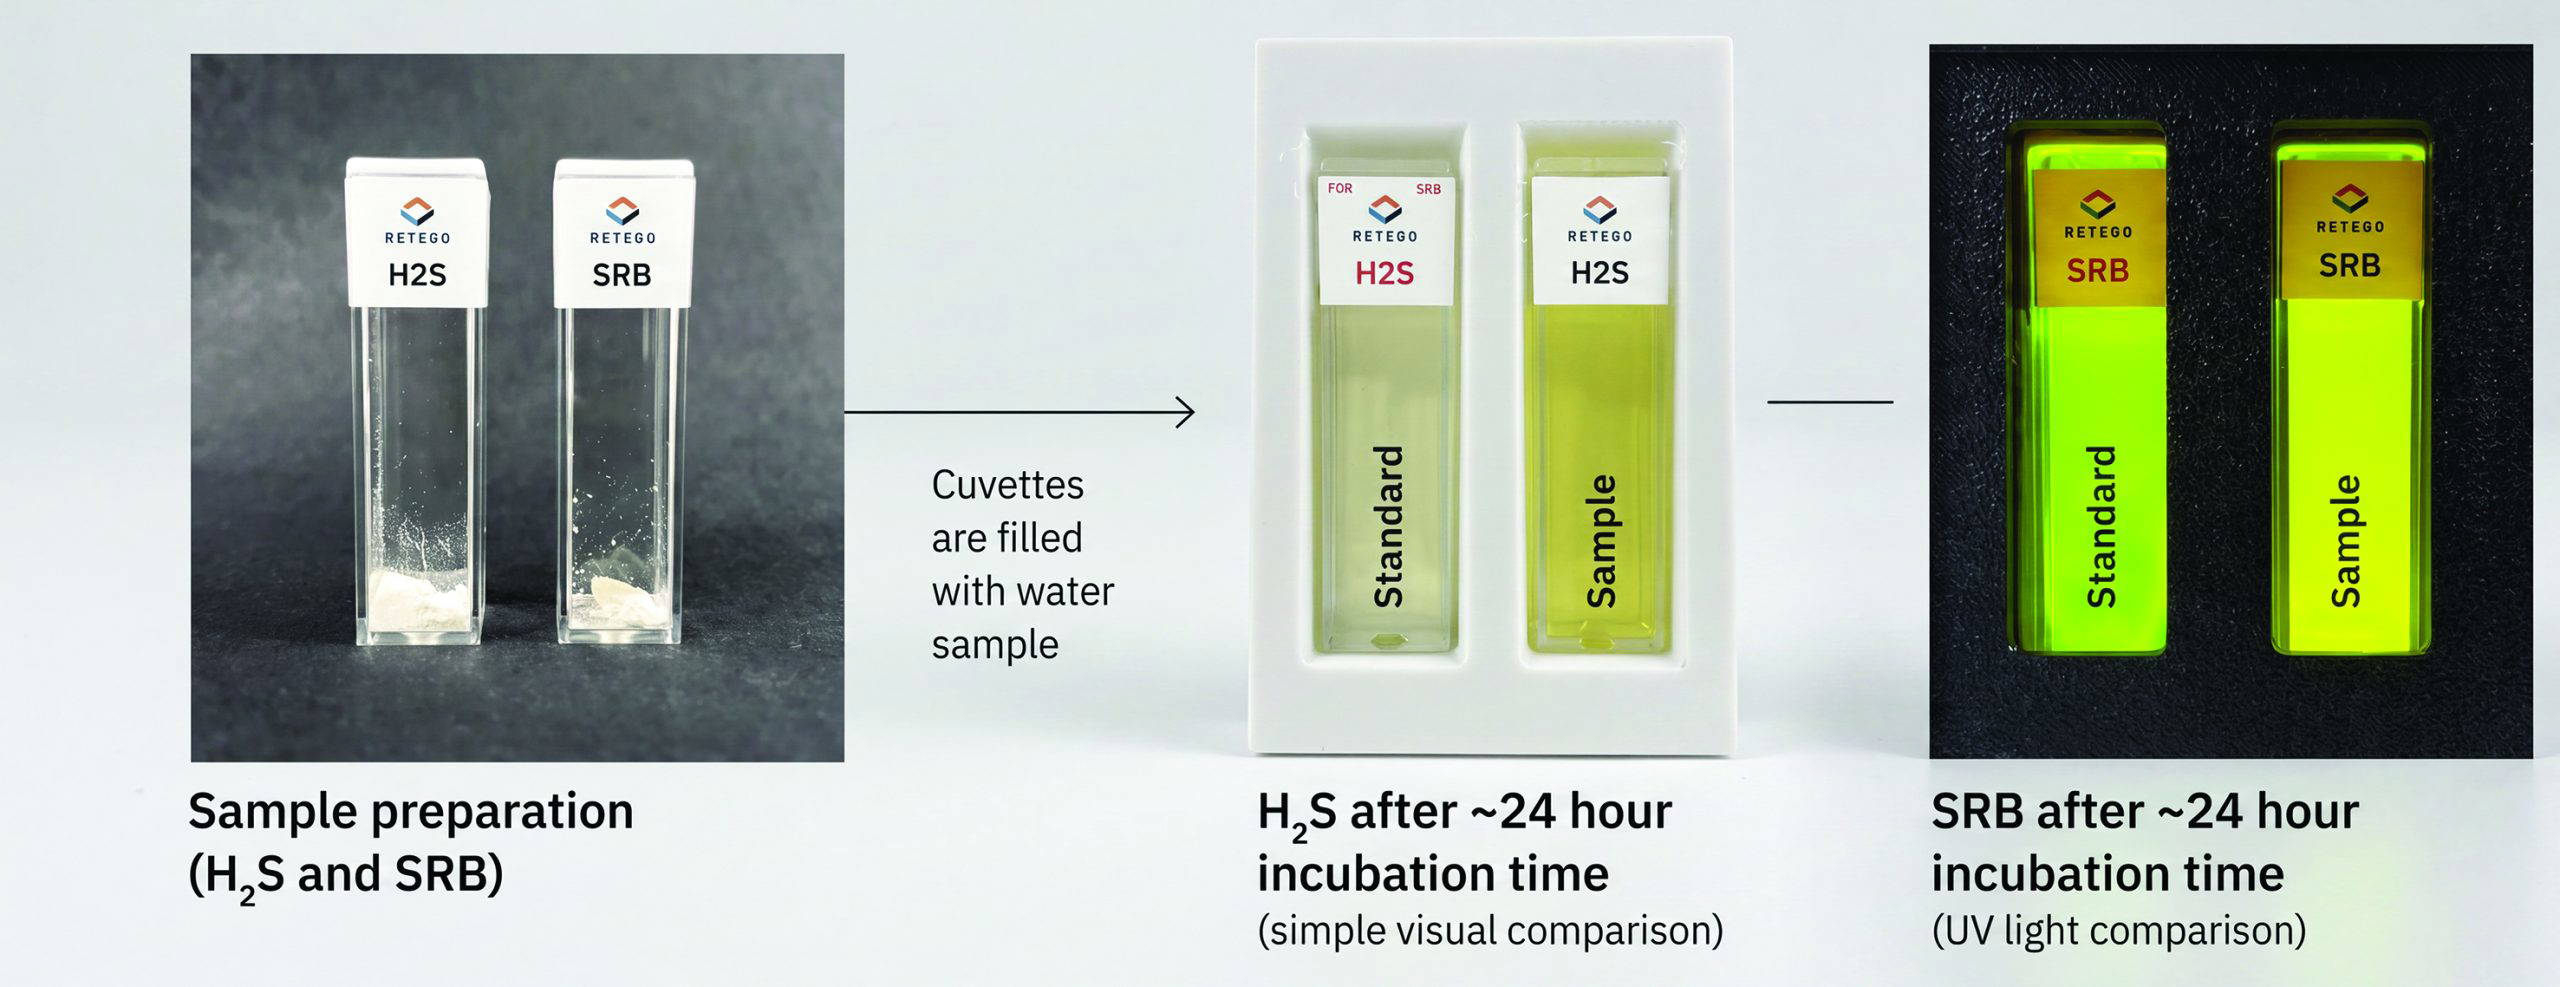
Figure 1. Workflow for rapid detection of sulphate-reducing bacteria (SRB) and associated hydrogen sulfide (H2S) in water samples. Following sample preparation, results are obtained between 1 and 24 hours, with visual indicators distinguishing microbial activity through colorimetric and fluorescent responses. This workflow illustrates how rapid detection enables earlier identification of microbial activity compared to traditional incubation-based methods.

Detection Time and Sensitivity

Field evaluations have demonstrated that this method can produce detectable results within approximately 1 to 24 hours, depending on bacterial concentration. Detection sensitivity has been observed at levels as low as 1,000 colony-forming units per milliliter of water (CFU/mL).

Field Application

The new method can be applied directly in the field and is effective across a wide range of water conditions, including variations in salinity and pH. Field-based testing reduces the need for sample transport and minimizes environmental impact on microbial activity prior to analysi

Validation and Comparative Performance

The new rapid SRB detection methods have been evaluated against established techniques, such as serial dilution and ATP-based testing across diverse environments, including Arctic, desert and tropical conditions. These evaluations demonstrate that rapid detection methods can provide results consistent with traditional techniques while significantly reducing time to result [6]. Faster turnaround enables more frequent monitoring and improved responsiveness.

Performance Characteristics

Key performance characteristics include:

• Detection sensitivity down to 1,000 CFU/mL
• Effective across a wide range of salinity and pH conditions
• Reduced likelihood of false-positive results
• Suitable for field-based application without
laboratory infrastructure
• Time to result typically between 1 and 24 hours

Limitations and Considerations

While the new rapid detection method provides significant advantages, several limitations should be considered. The method is specific to sulphate-reducing bacteria and does not detect other microbial groups, such as acid-producing bacteria. Additional testing may be required for comprehensive microbial analysis. Sample conditions are also critical. Fresh samples provide the most reliable results, while aged or oxygen-exposed samples may exhibit slower reaction times due to reduced microbial activity. Rapid detection methods should be used as part of a broader corrosion monitoring strategy that includes chemical analysis and system inspection.

Implications for Corrosion Management

The ability to detect SRB activity within hours rather than weeks has important implications for corrosion management. Operators can use rapid results to:

• Adjust treatment strategies, including biocide dosing
• Assess corrosion risk more quickly
• Identify microbial activity earlier
• Monitor effectiveness of bacteria mitigation programs • Provide early indication of reservoir souring

This supports a shift from reactive maintenance toward more proactive corrosion management.

Conclusion

Sulphate-reducing bacteria play a critical role in microbiologically influenced corrosion, yet traditional detection methods often fail to provide timely insight into their activity. Rapid detection approaches that target metabolic indicators offer a significant advancement in corrosion diagnostics. By reducing detection timelines from weeks to hours, these methods enable faster, more informed decision-making. As these technologies continue to evolve, they are likely to become an increasingly important component of modern corrosion management strategies and associated treatments. Regardless of the technique used, regular microbial monitoring is essential to evaluate whether preventative treatments are effective over time, as trend analysis provides the clearest insight into system conditions .

References

1. H Byars, Corrosion Control in Petroleum Production, 2nd ed. NACE International, Houston, TX, 1999, pp. 32–33.
2. D Enning and J Garrelfs, “Corrosion of iron by sulfate-reducing bacteria: New views of an old problem,”
Applied and Environmental Microbiology, 2014, 80(4). https://doi.org/10.1128/AEM.02848-13.
3. NACE TM0194-2014, Field Monitoring of Bacterial Growth in Oil and Gas Systems. NACE International, Houston, TX, 2014.
4. S A Hernandez et al., “ATP bioluminescence assay for onsite microbial assessment in drilling rig operations,” in Proceedings of the SPE/IADC Middle East Drilling Technology Conference, Abu Dhabi, UAE, 2018.
5. H S Khanfar et al., “Molecular approach for identifying and quantifying viable microorganisms using PMA-qPCR,” in Proceedings of the Middle East Corrosion Conference (MECC), 2025.
6. A Confer, J Fajt, K McLeroy and K P Ramirez, “Use of novel, rapid enzyme based assays to detect the presence of sulfate-reducing bacteria in oil and gas produced water,” Paper No. C2026-00198, in Proceedings of the AMPP Annual Conference and Expo 2026, AMPP, Houston, TX, 2026.

The Architecture, Mechanical Performance and Atmospheric Durability of a Triple Resin DTM Coating System

The Architecture, Mechanical Performance and Atmospheric Durability of a Triple Resin DTM Coating System

Jeremy Pasatta, Vice President of Technology, Advanced Polymer Coatings, Avon, OH, USA

Introduction

Industrial coatings face extreme and varied stressors: chemical exposure in processing facilities, ultraviolet light and weathering in outdoor service, vibration and impact in transport, and high humidity or temperature fluctuations in storage. Traditional solutions rely on multi-layer systems, each designed for a separate performance role. While technically effective, such systems introduce practical drawbacks: long cure times, complex application requirements, sensitivity to environmental variables, and risks of inter-coat adhesion failure.

Asset owners demand coatings that can perform multiple functions under real-world conditions across sectors such as rail transport, chemical processing, and heavy industry. Coatings must resist corrosion and chemical attack, remain flexible under vibration or thermal cycling, retain gloss and colour under UV light, and be applied efficiently in environments that may be less than ideal.

Advanced Polymer Coatings (APC) have developed a triple resin DTM (direct-to-metal) system to meet these evolving needs. This system merges the performance benefits of multi-coat structures into a single, co-cured architecture.

The triple resin coating system represents a deliberate shift away from this paradigm, integrating three distinct resin chemistries into a single film seeks to balance chemical resistance, mechanical toughness, UV durability, and rapid cure in one step. Co-curing ensures compatibility between components and creates a uniform polymer network with balanced properties. The result is a formulation designed not only for laboratory excellence but also for field reliability.

This paper integrates three complementary investigations of the system:

  1. Atmospheric Durability – assessment of UV stability, corrosion protection, chemical spot testing, and heat ageing.
  2. Mechanical Performance – using ASTM standards to evaluate adhesion, flexibility, and impact resistance.
  3. Performance Architecture – an in-depth look at resin selection, formulation strategy, and co-curing integration.

Atmospheric Durability of a Triple Resin DTM Coating

Materials and Test Methods

QUV Accelerated Weathering (ASTM D4587)

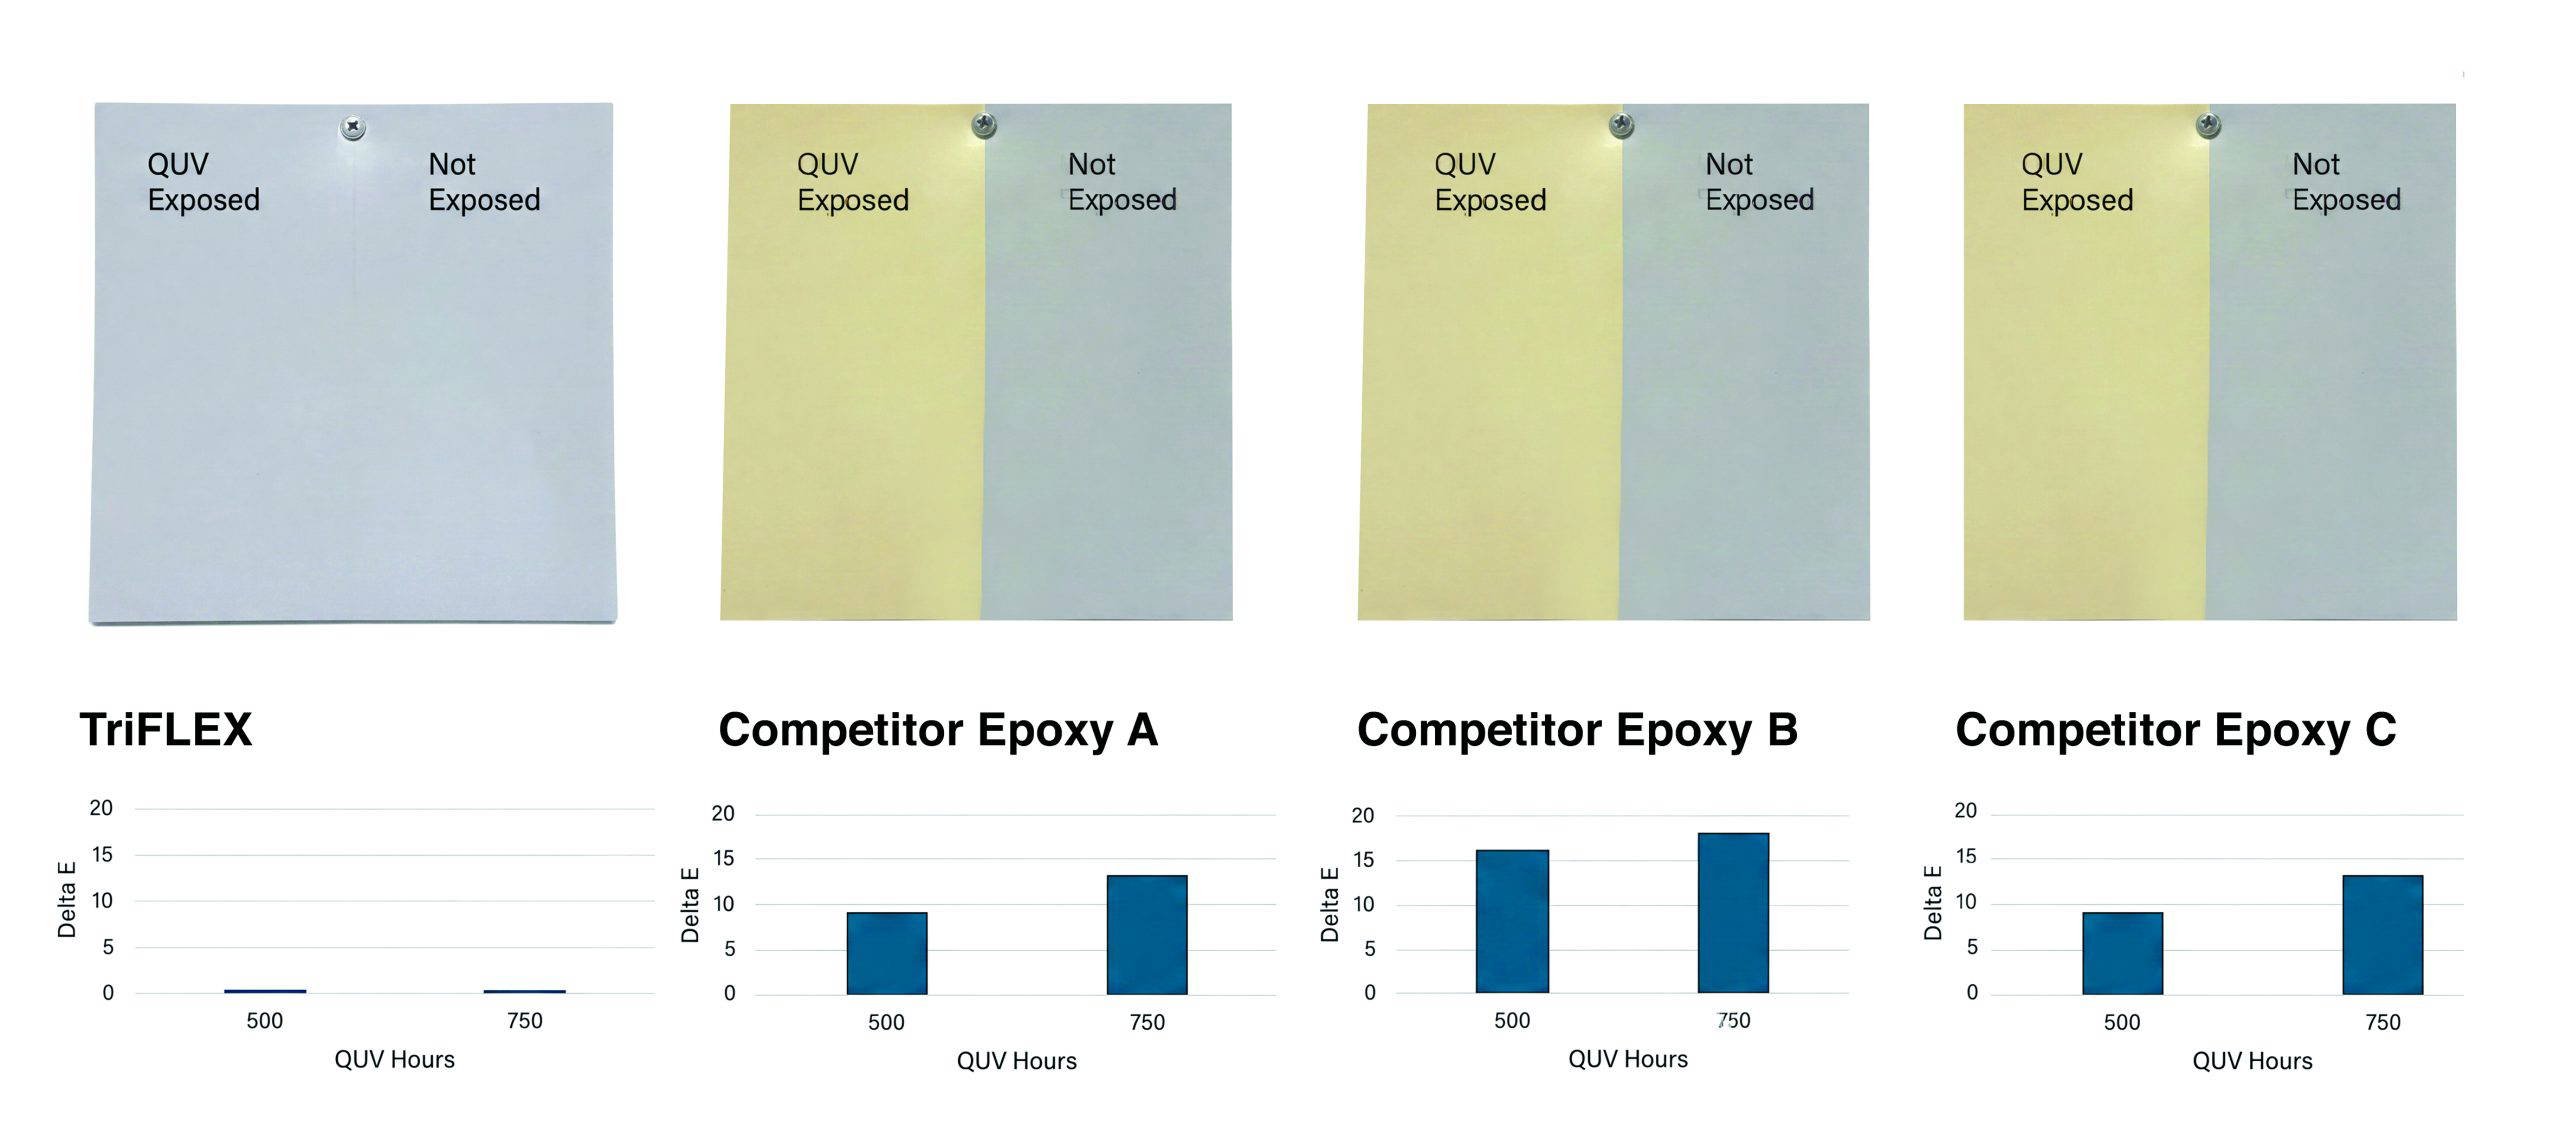
12” x 12” (30 x 30 cm) steel panels were sprayed with the triple resin coating system, along with three competitive epoxies. Each panel was partially masked to preserve an unexposed control area. Panels were subjected to 750 hours of UV exposure using UVA-340 bulbs. Colour stability was measured using Lab* colour space and Delta E calculations to quantify change.

Dry Heat Ageing (120°C, 720 Hours)

Performed by GPI Laboratories Project ID: N102301.B. The triple resin coating system panels were exposed to 120°C for 720 hours to simulate continuous high-temperature service. The post-exposure evaluation included visual assessment per ASTM D660 and D772 and adhesion testing per ASTM D4541.

Corrosion Testing (ISO 12944-6:2018)

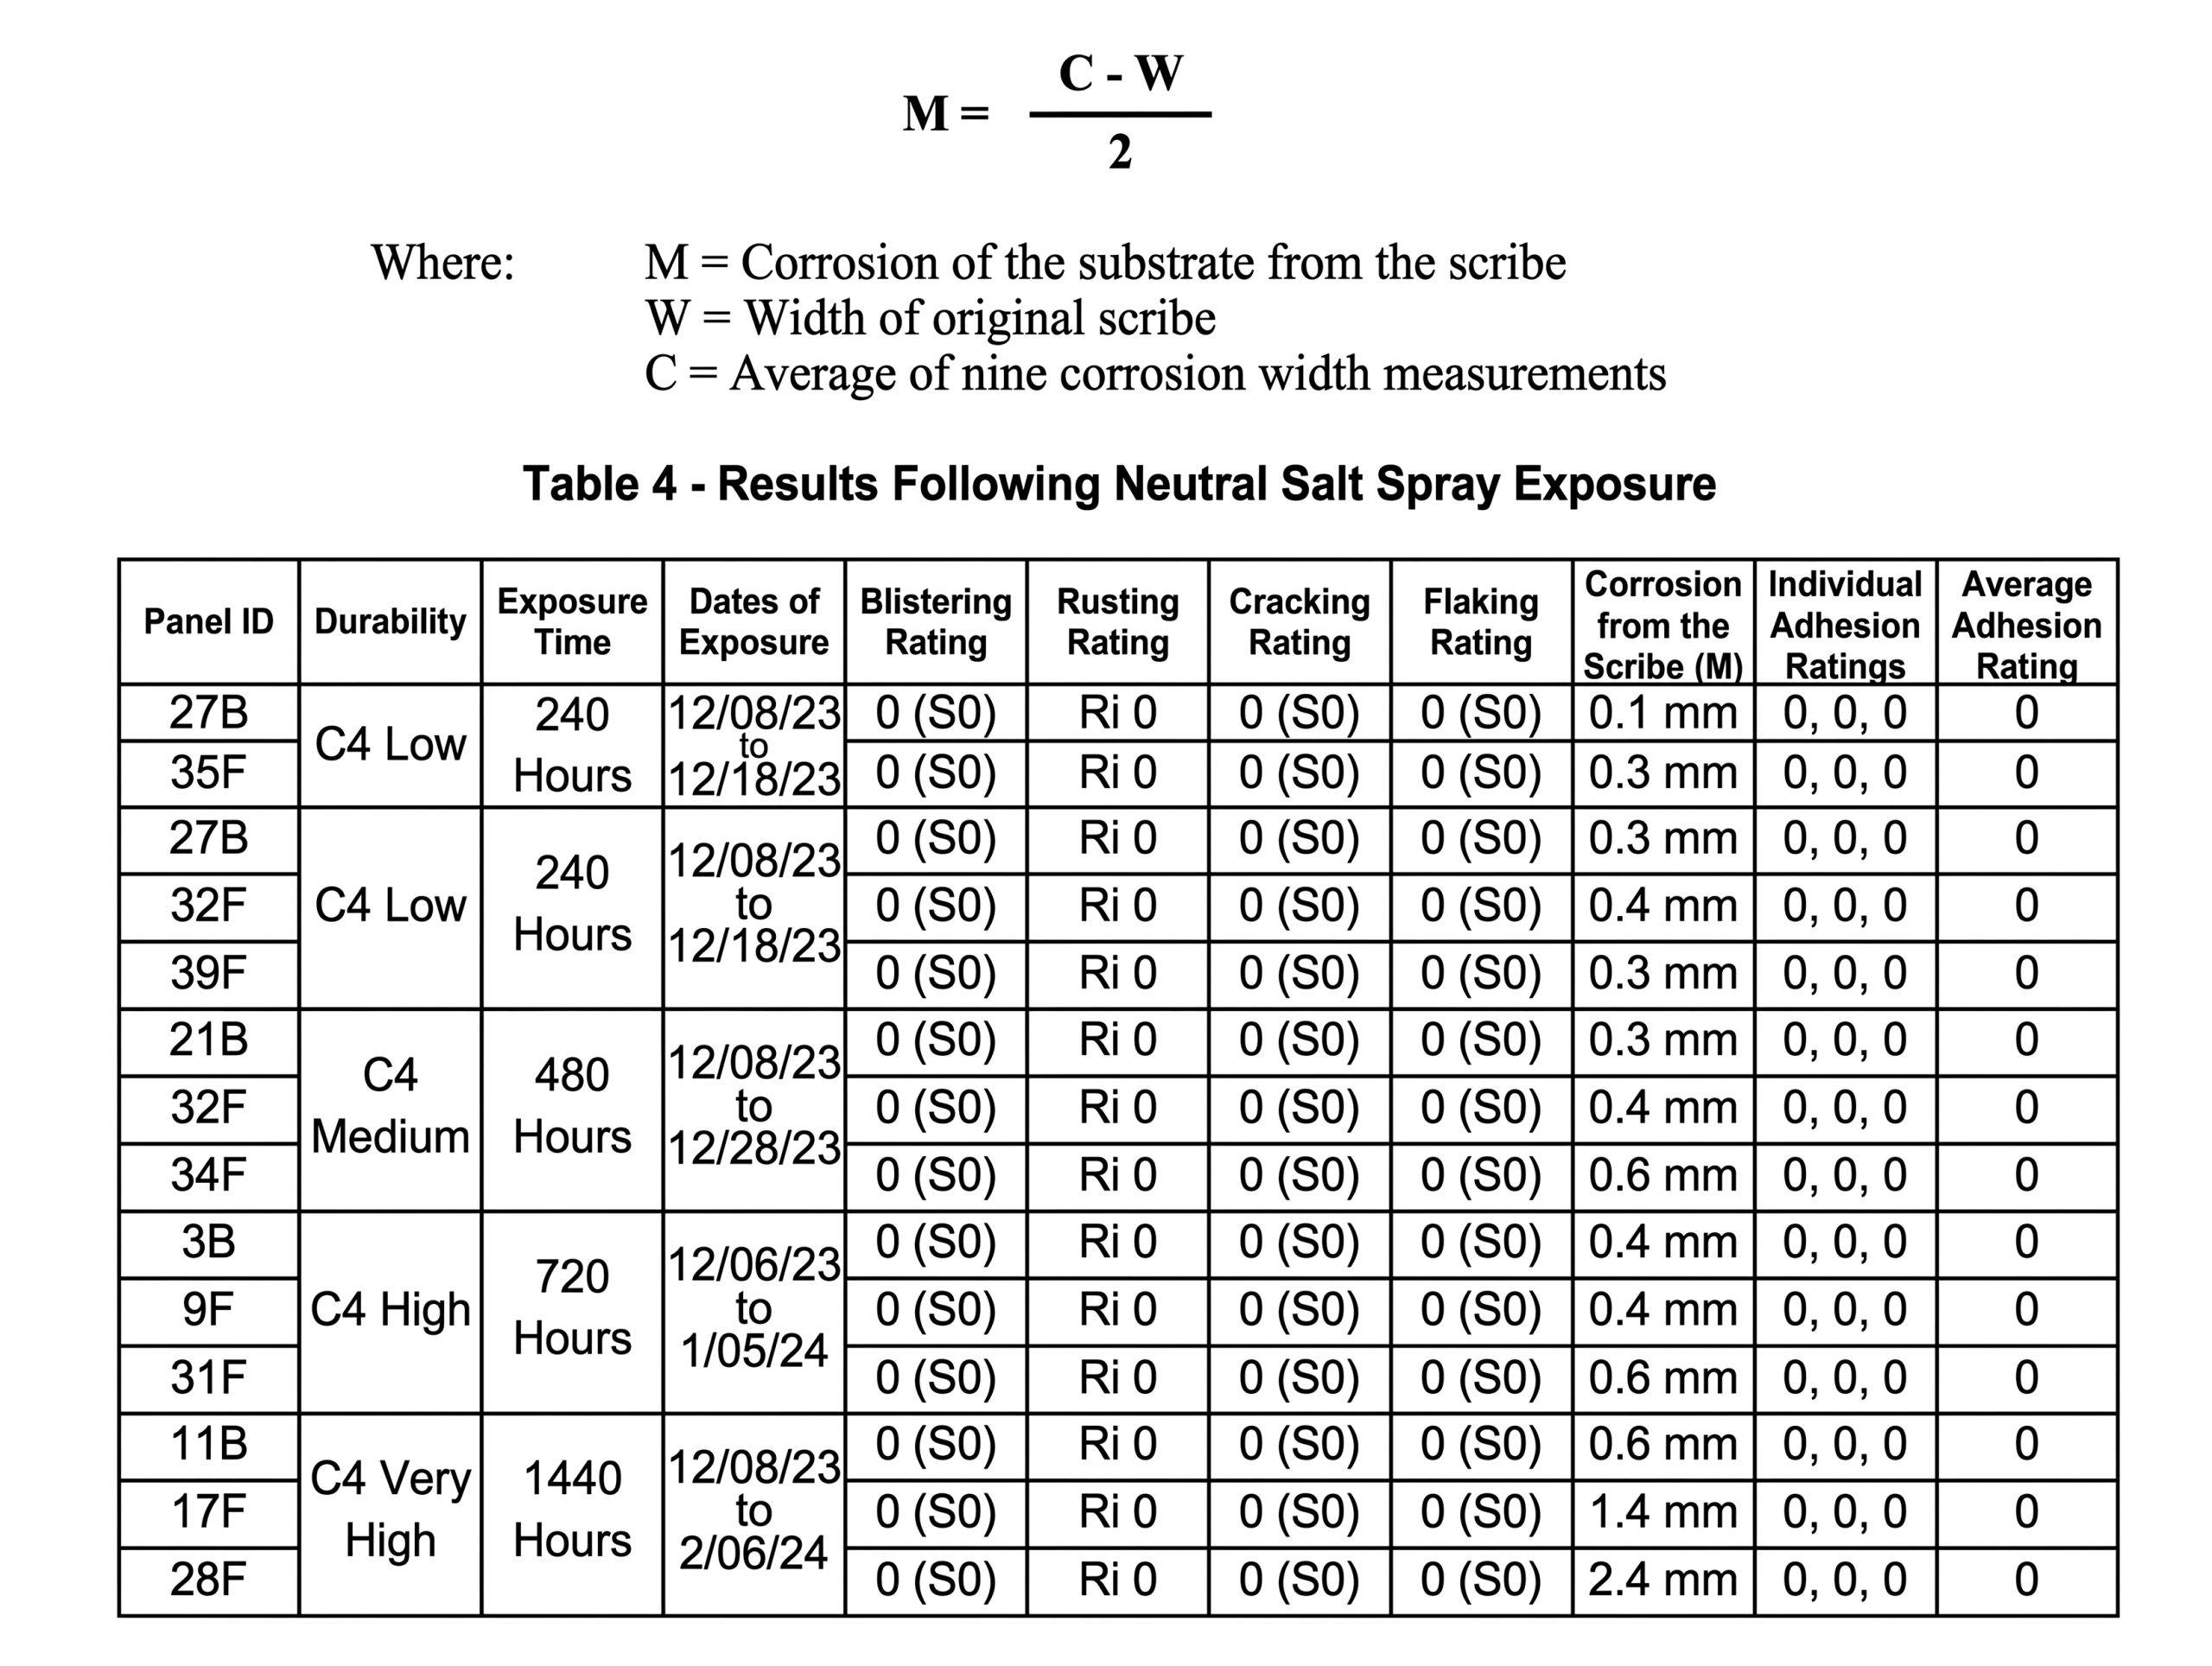
Performed by KTA-Tator, INC. Project No. 66075853-R2. Panels coated at 6.0-8.0 mils (150-200 microns) were subjected to salt spray (ISO 9227), humidity (ISO 6270-1), and cyclic ageing. Each test included multiple durability classifications from C3 to C4 (Low through Very High). The assessment included rusting, blistering, cracking, and scribe creep.

Figure 1: KTA-Tator, INC. Project No. 66075853-R2.

Chemical Spot and Humidity Testing (ASTM D1308, D2247)

Panels were exposed to ten aggressive chemicals for 72 hours at 23°C. The post-exposure evaluation included blistering (ASTM D714), rusting (ASTM D610), and visual degradation. Separate humidity exposure was performed at 38°C in 100% humidity for 1000 hours.

Spot and Spill Acid Resistance

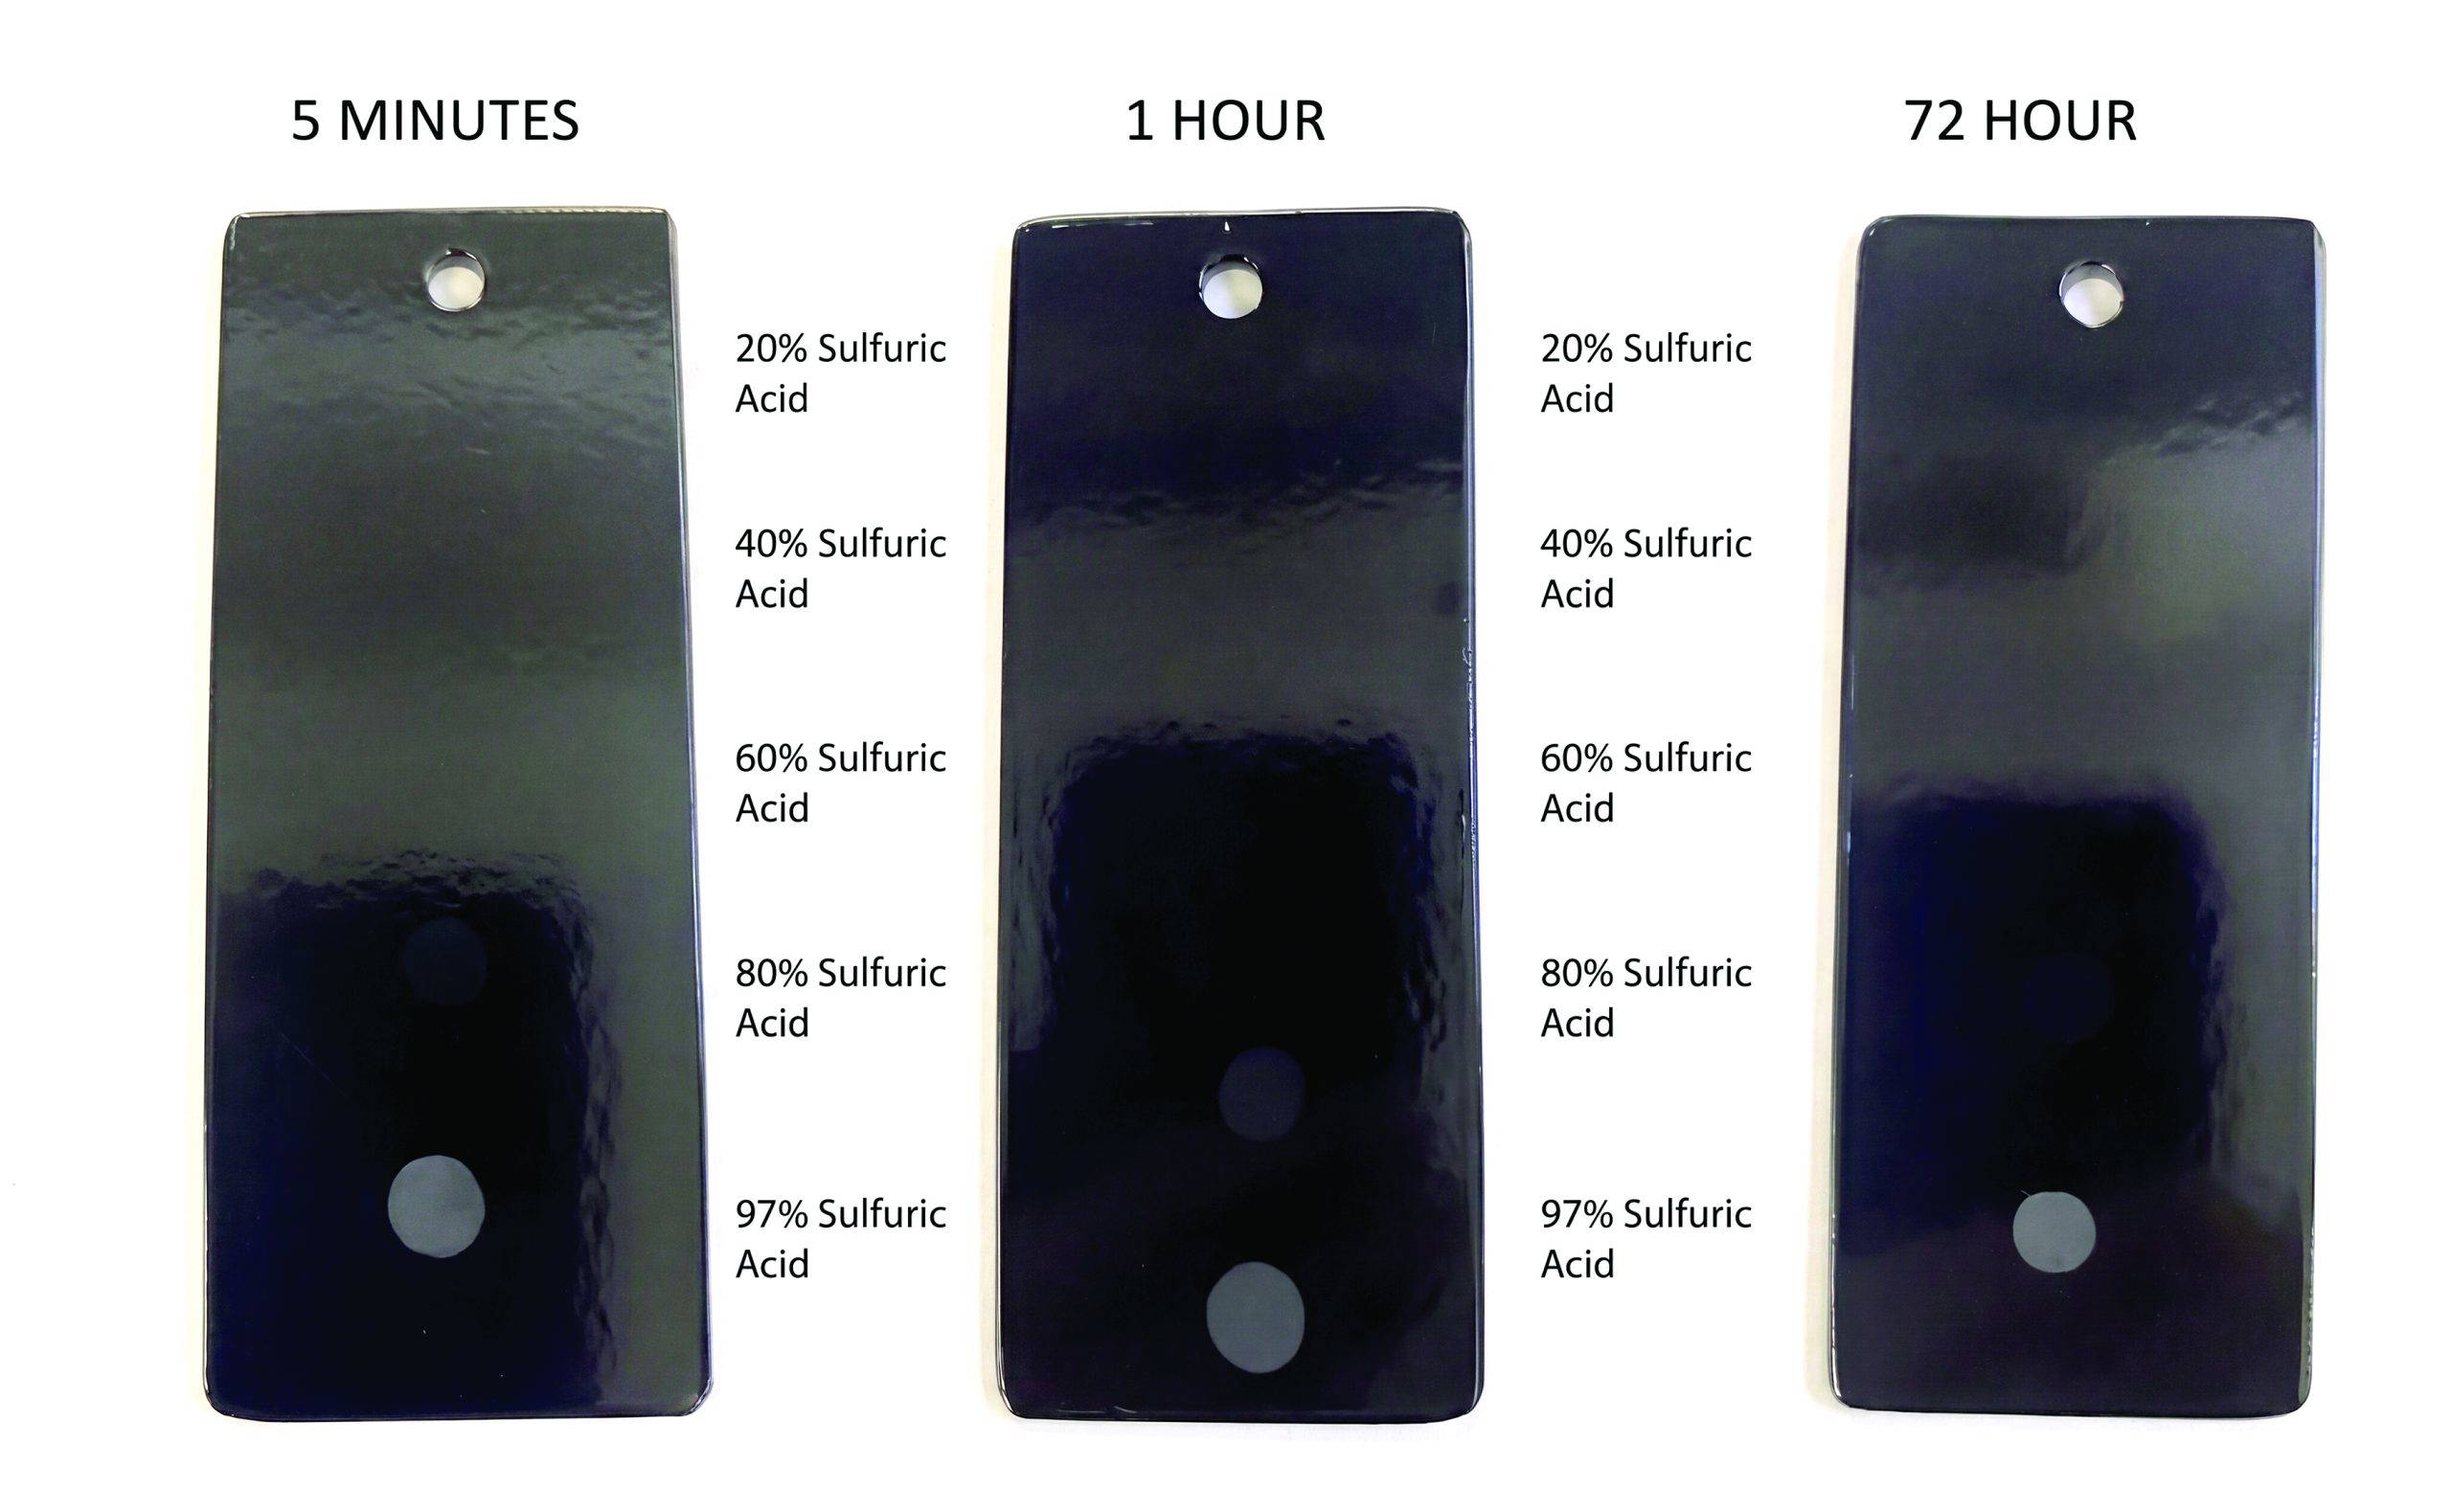
Panels were exposed to concentrated acids, including nitric, phosphoric, sulphuric, acetic, and hydrochloric, for up to 72 hours. Gloss loss, discolouration and film integrity were evaluated.

Results and Discussion

QUV Accelerated Weathering (ASTM D4587)

After 750 hours of UVA-340 exposure, the triple resin panels showed only minor discolouration and gloss loss compared to epoxies. Delta E measurements confirmed superior colour stability, highlighting its enhanced UV resistance. Masked panels directly compared exposed unexposed areas, demonstrating long-term aesthetic retention. This enhanced performance is considered due to UV-stable polyaspartic and polyurethane resins that absorb and dissipate radiation without the chain scission typical of conventional epoxies.

Figure 2: Results of QUV Accelerated Weathering (ASTM D4587) Testing at 500 and 750 Hours, Showing that TriFLEX Maintains Colour Stability with Minimal Change, While Competitor Epoxies A, B, and C Exhibit Significant Yellowing and Higher Values After Exposure.

Dry Heat Ageing Performance (120°C for 720 hours)

After prolonged exposure at 120°C, the triple resin system maintained structural and adhesive integrity, with no cracking, flaking or blistering. Adhesion exceeded 3600 psi, with cohesive rather than interfacial failure, suggesting strong thermal stability and possible cross-linking benefits. Minor discolouration and gloss loss were superficial, confirming suitability for continuous dry heat service up to 20°C.

Corrosion Resistance (ISO 12944-6:2018)

Corrosion testing by KTA-Tator, including salt spray, humidity, and cyclic aging per ISO 12944-6, showed the triple resin system met or exceeded C4 durability requirements. Panels exhibited no rusting, blistering, flaking, or cracking, and adhesion remained intact. Scribe creep was minimal and within limits, with only the most extreme accelerated regime causing higher creep than allowed. Overall, the results confirm the system as a reliable corrosion barrier for demanding coastal and industrial environments.

Chemical Spot and Humidity Resistance (ASTM D1308 and D2247)

The triple resin coating system strongly resisted aggressive chemicals, including concentrated acids and bases. After 72 hours of exposure, only minor gloss loss or surface yellowing was observed, with better retention of appearance and integrity than a leading epoxy. In 1000 hours of humidity testing at 38°C, panels exhibited minimal blistering, reduced underfilm corrosion, and superior adhesion.

These results confirm the system’s suitability for environments with frequent chemical contact and sustained moisture.

Figure 3: Results of Spot and Spill Acid Resistance Testing for TriFLEX™ Panels

Formulation Strategy and Resin Components

The foundation of this approach lies in the deliberate selection and chemical compatibility of three primary resins:

  • a Cyclic polyolefin-based polymer,
  • a Cycloaliphatic polyurethane, and
  • an Aliphatic polyaspartic (fast-curing, durable resin).

Each resin contributes to a specific performance domain, and together, they co-react to form a single crosslinked polymer network during cure.

Cyclic Polyolefin-Based Polymer

Serving as the primary barrier resin, the cyclic polyolefin-based polymer provides the dense, inert matrix necessary for chemical resistance and moisture impermeability. Unlike traditional epoxies, which often embrittle over time or under cyclic loading, this polymer retains its flexibility and integrity. Its molecular structure is characterised by tightly packed chains and minimal free volume, which translates into low water vapour transmission rates and high resistance to underfilm corrosion.

Cycloaliphatic Polyurethane

The second resin in the formulation is a cycloaliphatic polyurethane, chosen for its resistance to ultraviolet degradation and weathering. Derived from sterically hindered aliphatic isocyanates and UV-stable polyols, this polyurethane is chemically engineered to avoid the common pitfalls of aromatic variants, which degrade quickly under UV exposure.

Aliphatic Polyaspartic Resin

Completing the resin triad is an aliphatic polyaspartic resin formed by reacting a polyaspartic ester with an aliphatic isocyanate. This component offers several key benefits. First, it enables a rapid cure profile, reducing overall project timelines. Second, it is highly tolerant to humidity and temperature variations during application. These properties are particularly useful in real-world environments where conditions are rarely ideal.

Resin Integration Through Co-Curing

While each resin in the system offers unique attributes, the formulation’s performance depends on more than just its individual properties. Central to the system’s effectiveness is its co-curing behavior. Unlike traditional multi-coat systems, where each resin is applied and cured in isolation, the triple resin formulation is designed for simultaneous chemical reactions.

This co-curing strategy addresses several critical challenges. First, it prevents phase separation, a common issue when combining

chemically dissimilar polymers. The resins in this system are selected for their function and compatibility in terms of reactivity, polarity, and molecular weight distribution. Second, simultaneous cure minimises differential shrinkage and stress accumulation within the film. These unmitigated stresses can lead to cracking or delamination over time.

The result is a coating with a uniform modulus profile across the film thickness. This uniformity enhances both mechanical toughness and resistance to environmental degradation.

Furthermore, the system achieves a high crosslink density, improving chemical resistance and moisture impermeability. The balance of hardness and flexibility achieved through co-curing is especially significant, as most conventional coatings tend to favour one of these properties at the expense of the other.

Application and Performance Considerations

From a practical standpoint, this triple resin coating system is designed to perform in varied and unpredictable environments. Its moisture-tolerant cure behaviour, primarily driven by the polyaspartic component, allows for application under high-humidity or low-temperature conditions without introducing common defects such as amine blush or incomplete film coalescence.

The barrier properties of the cyclic polyolefin base bolster the formulation’s chemical resistance. At the same time, the cycloaliphatic polyurethane ensures surface durability in the presence of UV light, cleaning agents, and temperature fluctuations. The three resins contribute to a versatile performance profile that addresses the full range of chemical, mechanical, and aesthetic challenges commonly encountered in protective coatings.

In addition, the single-coat approach simplifies logistics. It reduces labour requirements, eliminates inter-coat inspection steps, and shortens turnaround time. This streamlined process is particularly advantageous in fast-paced project environments or settings where consistent environmental control is difficult.

Mechanical Performance of a Triple Resin DTM Coating

Materials and Test Methods

Adhesion Testing with Surface Conditioner

To evaluate the system’s adhesion to steel substrates under realistic surface conditions, carbon steel panels were prepared via dry abrasive blasting to a near-white metal finish (SSPC-SP10 / NACE No. 2). Panels were then exposed to three different pre-coating treatments:

  • No submersion (control)
  • Submersion in distilled water
  • Submersion in a 50:1 water dilution of HoldTight®102

HoldTight® 102 is a biodegradable, non-flammable surface preparation additive that removes soluble salts and prevents flash rusting post-blasting. Although widely used in field settings, its compatibility with high-performance coatings must be verified to ensure no adverse impact on adhesion.

After treatment, panels were coated with the triple resin coating system Grey at an average dry film thickness (DFT) of 8 mils (203 microns) and cured under ambient laboratory conditions (23 ± 2°C, 50 ± 5% RH) for seven days. Pull-off adhesion was tested per ASTM D4541 using an Elcometer 510 hydraulic adhesion tester with 20 mm aluminium dollies. Failure modes were classified as adhesive (at the substrate), cohesive (within the coating), or interfacial (between coating and dolly).

Flexibility Testing

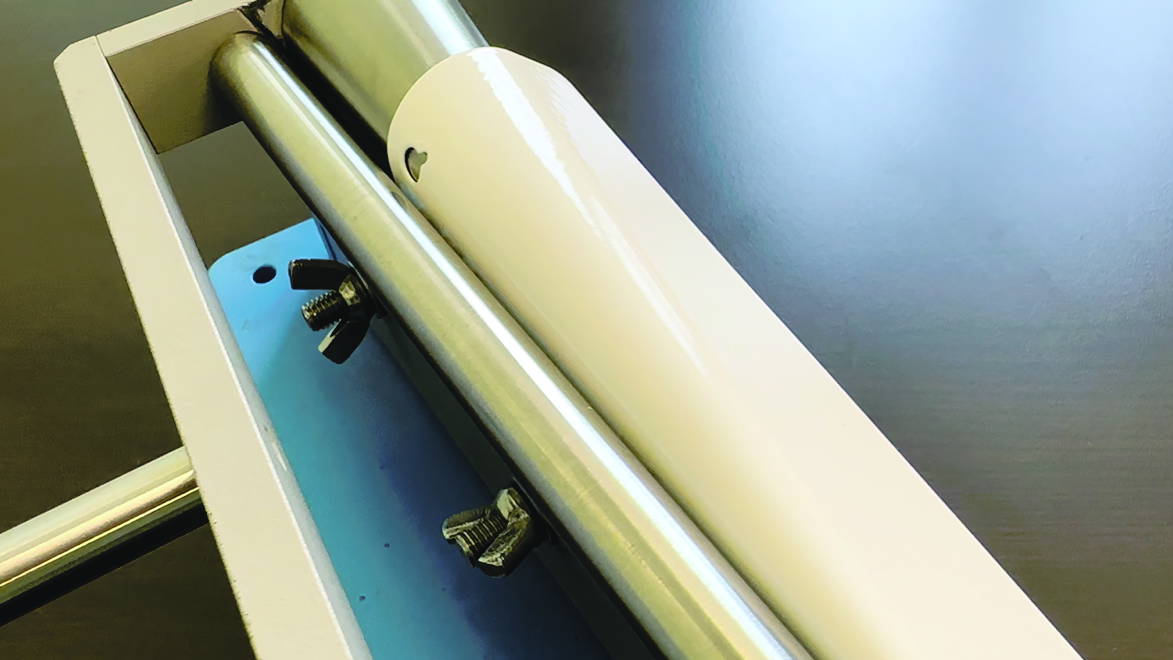
Flexural properties were assessed using the ASTM D522 Method A test for cylindrical mandrel bend. Coated panels were conditioned for 7 days post-application and then bent 180 degrees over mandrels of decreasing diameter, ranging from 1 inch (25.4 mm) to 1/8 inch (3.2 mm). The smallest mandrel diameter with no observed cracking was recorded. In parallel, a qualitative assessment of the coating’s crack resistance was performed by manually flexing fully cured panels back and forth to evaluate performance under repetitive bending stress, simulating flexural fatigue.

Figure 4: Mandrel Bend Test Performed on a TriFLEX™ Coated Panel.

Impact Resistance Testing

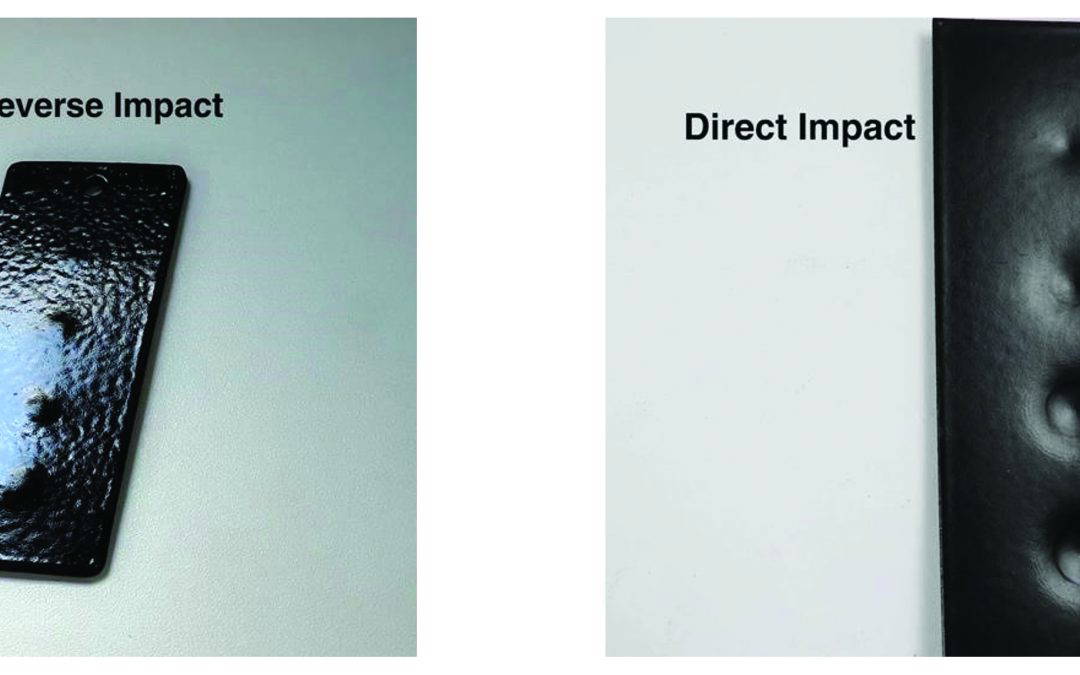
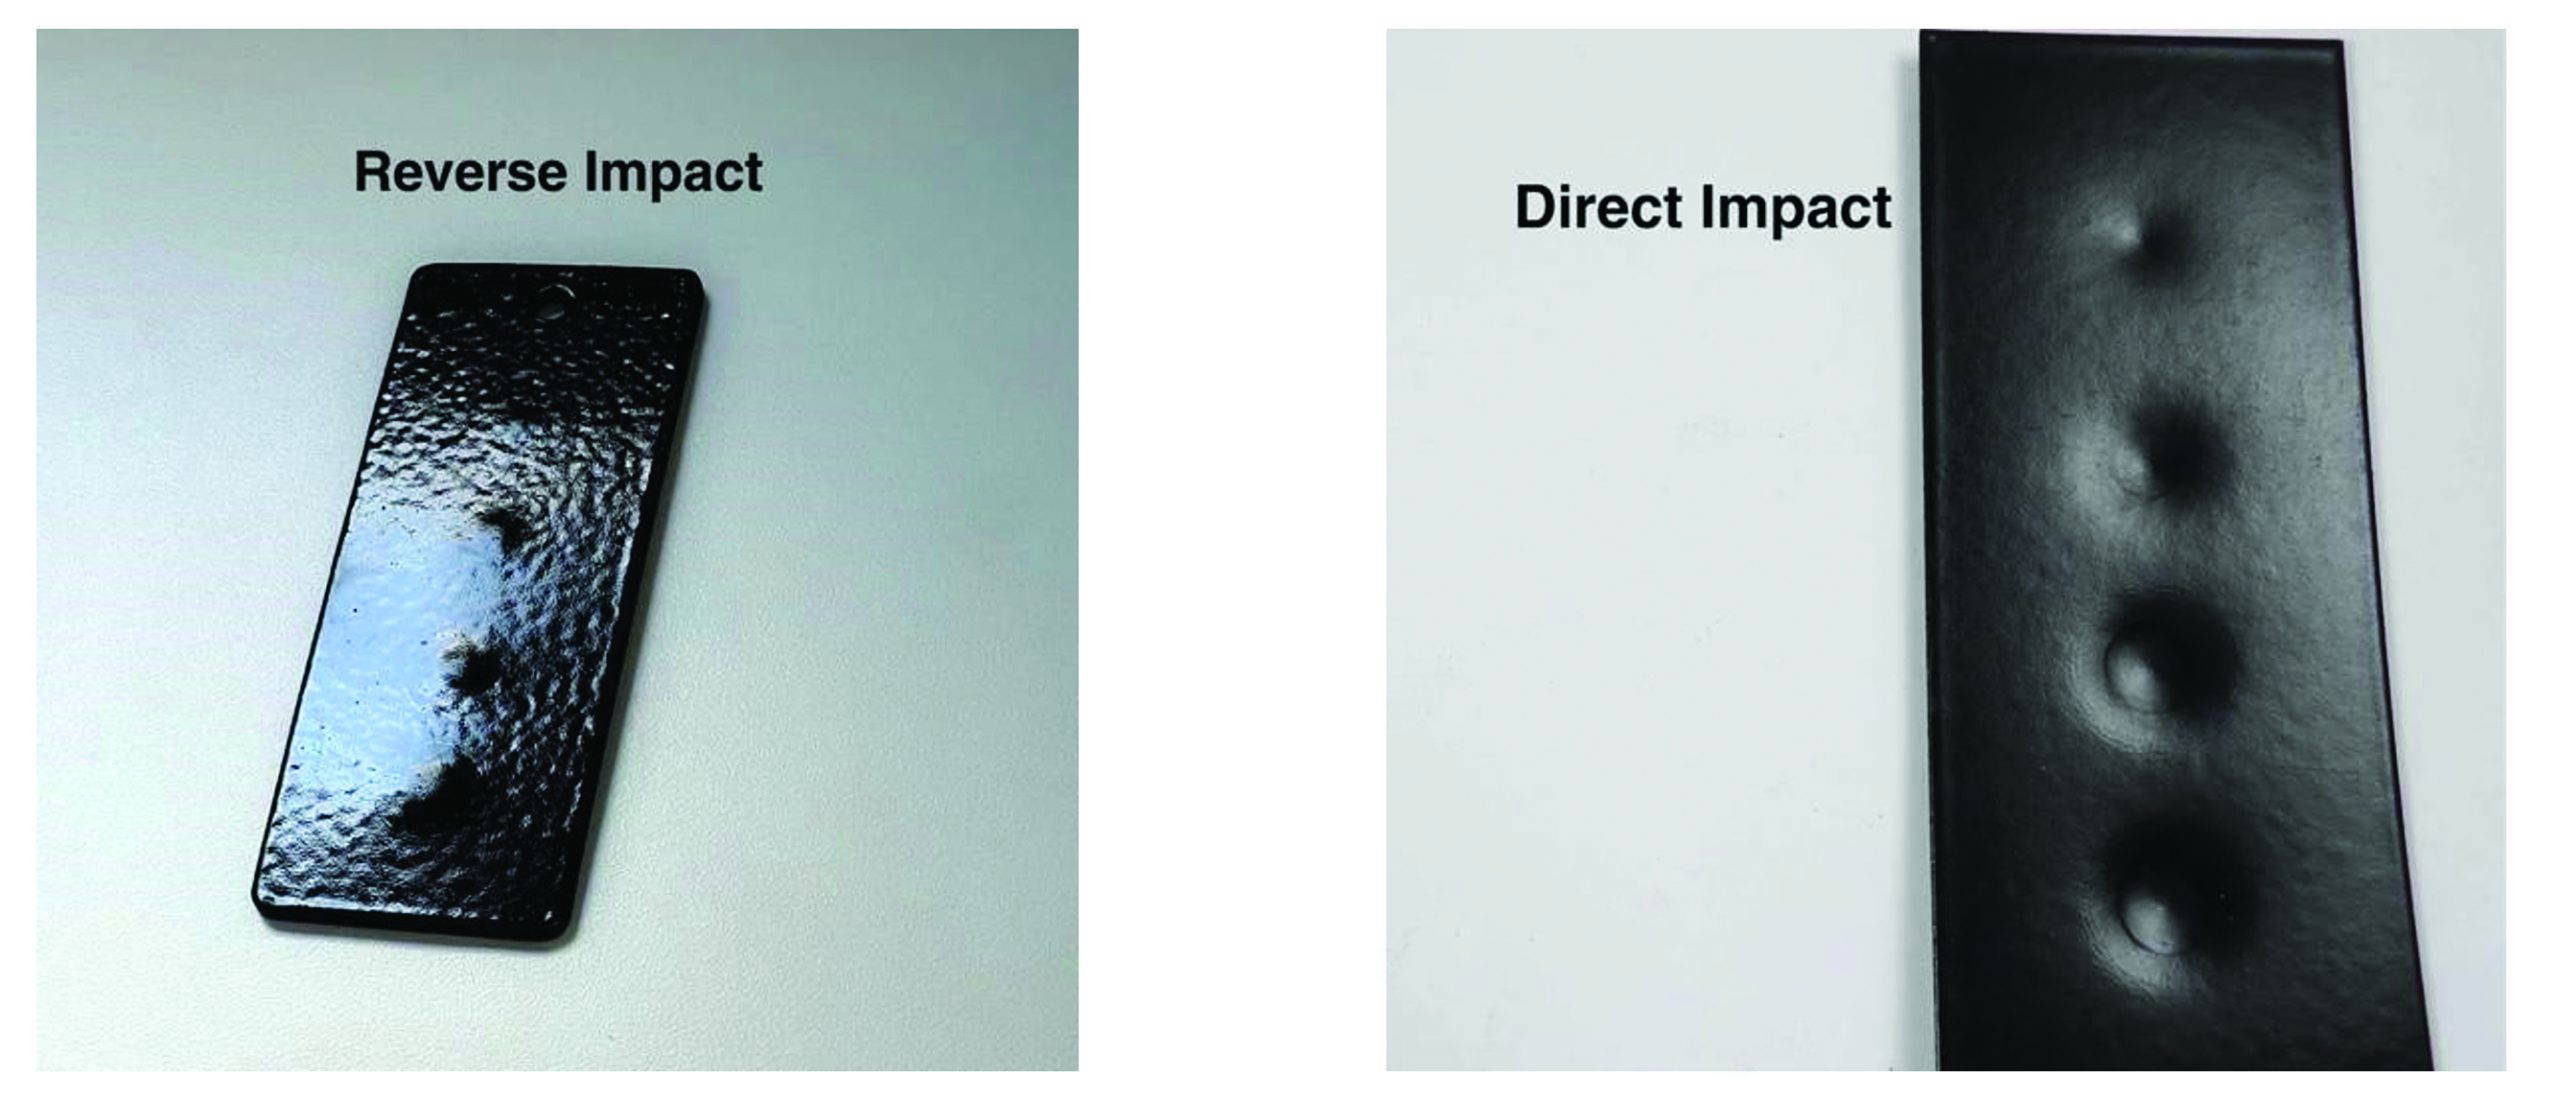
Impact resistance was evaluated by ASTM D2794, using a falling weight impact tester capable of delivering both direct and reverse impact. A hemispherical indenter was dropped from a fixed height to apply a known energy load (measured in inch-pounds) to the coated surface. For direct impact, the indenter contacted the coating directly. For reverse impact, force was applied to the uncoated backside of the panel. Failure was defined by visible cracking, delamination, or complete rupture of the coating film. The system’s results were compared to reference data from standard epoxy coatings.

Results and Discussion

Adhesion Performance

The average adhesion strength across all test conditions remained consistent. The control panel exhibited a pull-off strength of 1802 psi, while the distilled water-treated and HoldTight® 102-treated panels measured 1814 psi and 1796 psi, respectively. These differences are statistically negligible and fall within the expected variability of field-blasted substrates. More importantly, all tests exhibited cohesive failure within the system’s film, indicating that the failure occurred in the bulk material rather than at the substrate interface. This suggests that a

triple resin coating system establishes a robust bond to carbon steel surfaces and maintains interfacial strength even in salt removal agents or residual moisture films. Field use of HoldTight® 102 as part of the surface preparation process does not compromise adhesion and may be confidently included in standard surface treatment protocols.

Flexibility Results

The triple resin coating system demonstrated high flexibility, withstanding 180-degree bending over a 1/8-inch mandrel without cracking, delamination, or visible film degradation. This performance equates to an elongation threshold exceeding 30%, which surpasses the flexibility range typically observed in conventional epoxies (6% to 12%).

The triple resin matrix appears to distribute mechanical stress across the film, reducing localised strain concentrations that would otherwise initiate cracks. When manually flexed in both directions, panels retained film integrity, supporting that the system possessed static flexibility and dynamic strain tolerance. These attributes make the coating advantageous for mechanical vibration, thermal cycling or structural movement environments.

Results of Mandrel Bend Test Performed on a TriFLEX™ Coated Panel.

Impact Resistance

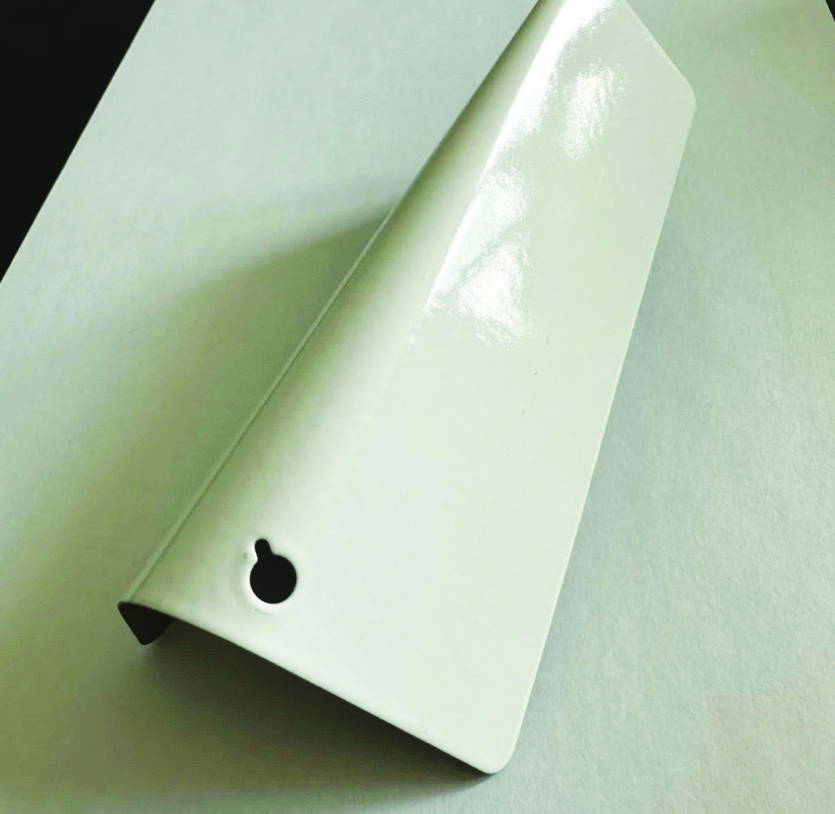
Results from ASTM D2794 testing showed that the triple resin coating system provides impact resistance values exceeding 160 in-lb for both direct and reverse impacts. Conventional epoxy coatings typically register direct impact resistance in the 70 to 90 in-lb range and show significantly diminished resistance in reverse impact due to their brittleness.

The coating’s ability to absorb and dissipate mechanical energy from both directions without cracking or film failure reflects the synergistic effect of its resin composition. This makes it well-suited for highwear environments where equipment may be subjected to dropped tools or shifting loads. The dual-mode impact resistance also suggests that the coating can provide reliable protection during service, fabrication, transport and installation.


Figures 6: Results of Revers Impact and Direct Impact ASTM D2794 Testing of TriFLEX™ Panels.

Conclusion

This research indicates significantly improved performance traditionally reserved for multi-coat architectures through uniting three distinct resin chemistries into a co-cured single-coat system. The performance architecture study established the scientific rationale for resin selection and integration. The mechanical study confirmed that adhesion, flexibility, and impact resistance exceed conventional epoxy benchmarks. The atmospheric research validated resilience against UV, corrosion, humidity, heat, and chemical exposure.

Together, these results confirm the developed triple resin coating system as a durable, versatile, and efficient solution for industrial and transportation applications, offering asset owners the ability to reduce downtime, simplify coating application, and extend protection cycles.

Bilfinger Secures Offshore and Onshore Maintenance Contracts in the UK

Bilfinger Secures Offshore and Onshore Maintenance Contracts in the UK

Bilfinger has secured two significant maintenance contracts in the UK, strengthening its presence across both offshore and onshore energy infrastructure. The awards include work on the Cygnus gas field for Ithaca Energy and a fabric maintenance contract at the SAGE Terminal in St Fergus with Wood plc.

The first contract covers Access and Fabric Maintenance Services for Ithaca Energy’s Cygnus assets. The Cygnus gas field is the UK’s largest producing gas field and plays a key role in supporting national energy security. The development comprises three bridge-linked Alpha platforms and connects to the Bacton Gas Terminal, operated by Perenco.

The field also includes Cygnus Bravo, an unmanned satellite platform located around 7 km northwest of Cygnus Alpha. The contract follows Ithaca Energy’s acquisition of Eni’s UK upstream oil and gas assets in 2024, which added the Cygnus field to its North Sea portfolio. In a second award, Bilfinger will deliver Fabric Maintenance and Access Support Services at the SAGE Gas Terminal under a contract with Wood plc. The three-year agreement marks a return for Bilfinger to the strategically important site and further strengthens its operational footprint in the region.

As part of the project, Bilfinger will introduce product and digital innovations to support continuous improvement. This includes consolidating operational data onto a digital platform, introducing new corrosion protection products, and leveraging group-wide capabilities for prefabricated insulation solutions.

Sandy Bonner, President Western Europe at Bilfinger, said the contract wins reinforce the company’s strong position in the UK energy sector and highlight the value of its integrated services model for customers operating critical infrastructure.

Source: https://www.bilfinger.com/en/

Bilfinger Secures Major NDT Inspection Services Contract with bp

Bilfinger Secures Major NDT Inspection Services Contract with bp

Aberdeen, United Kingdom – International industrial services provider Bilfinger has been awarded a significant contract to deliver Non-Destructive Testing (NDT) inspection services across all of bp’s North Sea assets.

This new award builds on the longstanding collaboration between the two companies and follows the recent three-year extension of Bilfinger’s insulation, access and painting (ISP) contract with bp in the UK, which was first secured in 2019.

Under the agreement, Bilfinger will deploy a wide range of advanced inspection technologies, including robotics and artificial intelligence, to enhance asset integrity management. These solutions are designed to increase efficiency, improve safety, and reduce carbon emissions, supporting bp’s wider commitment to sustainable offshore operations.

A key feature of the contract is the introduction of a fully integrated, end-to-end digital workflow. This approach aims to transform inspection practices by enabling real-time data management, streamlined reporting, and AI-ready integration. By embracing smart digitisation, Bilfinger will deliver inspection services that not only meet but exceed industry expectations for reliability and sustainability.

The expansion of service scope across the North Sea assets demonstrates bp’s continued confidence in Bilfinger’s capability to provide safe, efficient, and innovative solutions. It also reinforces Bilfinger’s position as a trusted partner for the oil and gas industry in the UK continental shelf.This latest contract strengthens the company’s portfolio of asset integrity and inspection services, ensuring the continued safe operation of critical offshore infrastructure in one of the world’s most mature oil and gas regions.

Source: https://www.bilfinger.com/

Hexigone and Alfaa Chem Join Forces, to Bring Advanced Anti-Corrosion Technology to the GCC Market

Hexigone and Alfaa Chem Join Forces, to Bring Advanced Anti-Corrosion Technology to the GCC Market

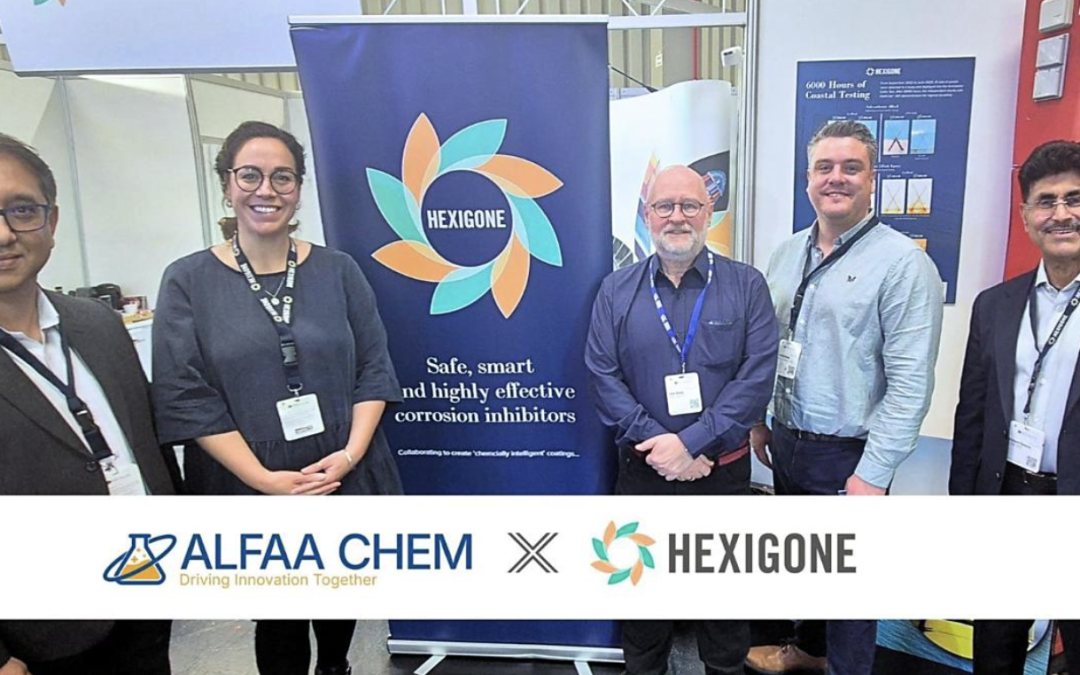
Hexigone Inhibitors Ltd, a UK-based innovator in smart corrosion inhibitors, has entered a strategic partnership with Alfaa Chem, a leading chemical distributor in the Middle East. The collaboration aims to deliver high-performance anticorrosion technologies to the Gulf Cooperation Council (GCC) region, offering coating manufacturers the ability to differentiate their products as well as reduced formulation costs.

This partnership marks a major step forward in the supply of advanced materials to the region’s anti-corrosion coatings sector, particularly targeting applications in construction, oil and gas, and infrastructure maintenance.

Hexigone’s unique Intelli-ion® technology https://www.hexigone.com/whats-new/do-more-for-less-with-intelli-ion-elevating-anti-corrosion-coatings-with-low-loadings

can be used at very low loadings alongside traditional inhibitors like zinc phosphate, significantly reducing the total inhibitor content required in a formulation. This co-blending approach maintains high corrosion protection while enabling a reduction in overall film thickness—helping to streamline application processes and, in many cases, eliminate the need for brush blasting during structural steel maintenance.

Founded in 2004, Alfaa Chem is a well-established chemical distribution company with a strong presence across the UAE, Saudi Arabia, and beyond.

“Partnering with Hexigone represents a forward-thinking move for both our companies and for the region’s coatings industry,” said Richard D’Souza, Technology Director at Alfaa Chem. “Their smart inhibitor technology addresses multiple industry challenges—ranging from performance under severe environments like C5+ conditions to improving adhesion on galvanized and thermally sprayed steel. Together, we aim to support formulators in transitioning away from zinc-rich and chromate-based systems toward more sustainable and cost-effective solutions.”

This partnership positions both companies to meet rising performance expectations while promoting safer, more environmentally conscious technologies—all while helping manufacturers achieve meaningful reductions in formulation costs.

About Alfaa Chem
Headquartered in Sharjah, UAE, Alfaa Chem is an independent chemical distribution company serving the Middle East, USA, and Africa. With warehousing in Sharjah, Dubai, and Saudi Arabia, the company supplies specialty chemicals across various sectors and prides itself on its commitment to quality, innovation, and exceptional customer service.

About Hexigone Inhibitors Ltd
Based in Port Talbot, UK, Hexigone is at the forefront of corrosion inhibitor technology. Their flagship products offer enhanced corrosion protection and sustainability for protective coatings, providing a compelling alternative to traditional materials.

Media Contact
ella.newington@hexigone.com
+44 (0)1792 439 422
www.hexigone.com


Hexigone Case Study: Holyhead Train Station

Hexigone Case Study: Holyhead Train Station

Project Background

Holyhead station, a prominent railway station situated in Wales. Strategically located near a harbour and high street, it serves as a key transport hub, seamlessly connecting the region’s rail and maritime networks. Situated on the harbour, the Grade II listed train station has endured persistent exposure to salty sea air, high humidity, heat from the trains and diesel fumes. This relentless environmental assault has resulted in significant corrosion of the structural steel canopies, causing progressive deterioration of the exposed steel.

The Challenge

Network rail’s current coatings manufacturer could not guarantee their product’s effectiveness due to the harsh location. They needed to find an enhanced paint system that outperforms the currently specified paint system to: Maintain structural integrity Preserve the station’s historical features Reduce maintenance and repair costs.

Solution  

The solution implemented was Hexigone’s “smart” corrosion inhibitor, Intelli-ion® AX1, chosen for its superior corrosion protection in harsh environments. Achieving C5-level corrosion resistance, AX1 effectively combats corrosion in highly aggressive environments, such as coastal areas, while delivering longer-lasting corrosion protection. Intelli-ion® AX1 has also endured 1440 hours in salt spray testing (ASTM B117), and offerred enhanced adhesion and colour retention in both laboratory and live testing.

Methodology

To compare performance, two protection systems were applied simultaneously:
• 50% of the train station was painted with astandard system.
• 
The remaining 50% was painted with a system enhanced 
with Intelli-ion®

Laboratory Test Results

Panels with both standard paint and paint enhanced with
Intelli-ion® AX1, were tested side by side. The addition of AX1 improved corrosion resistance, significantly increased adhesion levels and the bonding of the aluminium primer to the metal surface. 1000 Hours Salt Spray ASTM B117.

Real-World Results

The addition of intelli-ion® AX1 significantly enhanced the 50% repainting process of the mile-long station’s surface, comprised of tool-prepared Victorian cast iron. Contractors observed the following improved application properties; “the paint applied more easily, spread more evenly, and provided more coverage.” By enhancing surface tolerance, AX1 improved adhesion by 163.16%, resulting in a 33% increase in performance. This improvement led to reduced maintenance requirements, delivering a highly efficient, cost-effective solution with enhanced long-term asset protection.

3 Years After Application

Intelli-ion® AX1 demonstrated superior performance compared 
to the standard system – designed to provide 15 years of 
corrosion protection.