Ahmad Usman, Group Innovation R&D Engineer, Welding Alloys Group UK
Meet The Author
Ahmad Usman is a Group Innovation R&D Engineer at Welding Alloys Group UK, specialising in high-temperature material degradation in demanding industrial environments. He works with a multidisciplinary team to design alloys that resist corrosion and wear in heavy industry applications. His expertise in thermal spray coatings enables him to address complex challenges through practical, performance-driven solutions. His work focuses on real-world case studies to develop materials that protect critical components and extend service life under extreme conditions.
Ahmad is part of a global research and innovation team committed to technical excellence and supporting industrial partners in advancing their products and services. His research interests focus on the future performance of materials in increasingly aggressive operating environments.
Introduction
Material degradation at high temperature remains a critical challenge across a wide range of industrial sectors, including chemical processing, aerospace, gas turbines, energy generation, refining and petrochemical processing, and metallurgical operations (Spiegel, Zahs, and Grabke 2003). Components operating under such conditions are exposed to reactive gaseous and condensed species, leading to reduced operational efficiency, increased maintenance demands, and ultimately premature component failure. These challenges carry significant economic
and operational consequences, underscoring the importance of understanding and mitigating high-temperature degradation processes (Khantisopon et al. 2022).
The nature and severity of degradation are strongly influenced by the local chemical environment, which is governed by factors such as process conditions, feedstock composition, and deposit chemistry (Corrosion Basics Understanding the Basic Principles and Causes of Corrosion
n.d.). In oxygen-rich environments, protective oxide scales may form and provide a degree of resistance; however, under oxygen-deficient conditions, the stability of such layers is compromised, increasing susceptibility to accelerated attack. The presence of sulphur- and chlorine-containing species further complicates these processes by introducing additional degradation pathways (Floreen and Kane n.d.). Sulphur-rich environments typically promote sulphide formation, while chlorine-containing species can induce active oxidation through the formation and volatilisation of metal chlorides, resulting in rapid material loss (Sadeghimeresht et al. 2018; Usman et al. 2025).
In practical systems, these mechanisms rarely occur in isolation. Instead, they evolve dynamically in response to local variatio in temperature, gas composition, and deposit accumulation, as shown in Figure 1 (Usman et al. 20 As a result, degradation behaviour is often highly heterogeneous, even within a single system, making material selection and lifetime prediction particularly challenging.
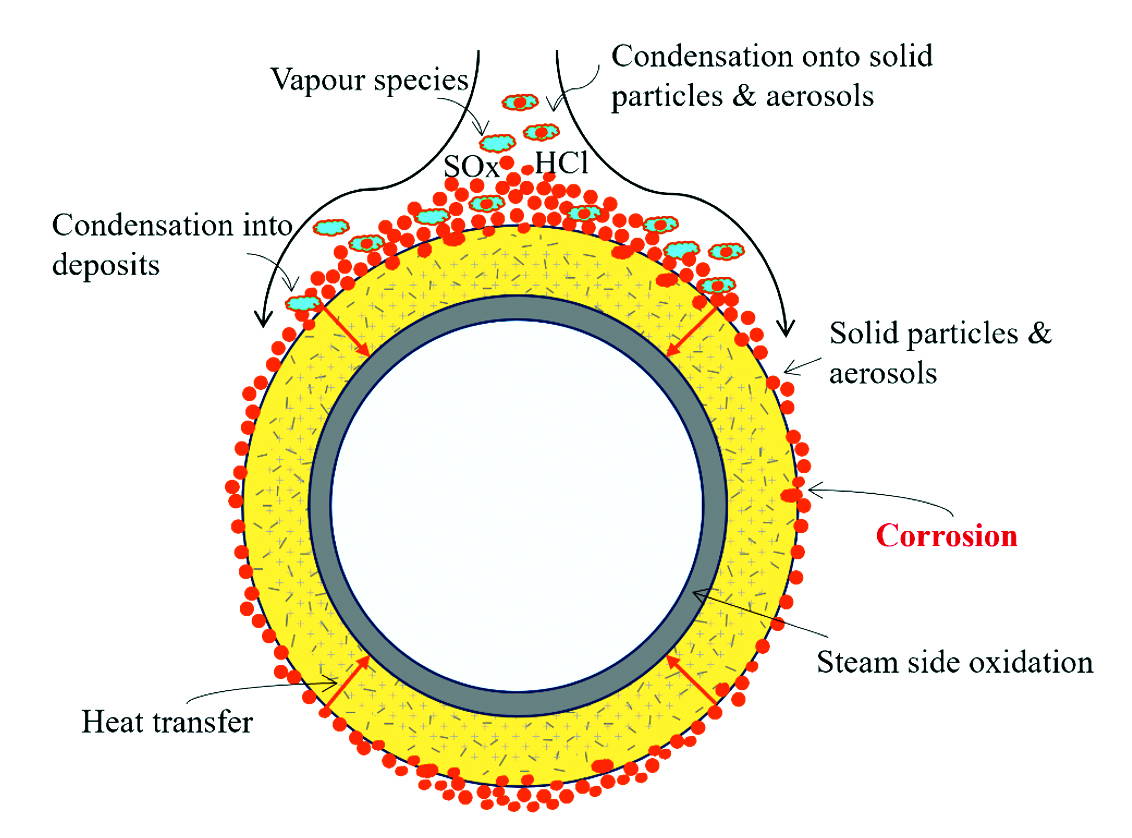
Figure 1: Schematic Representation of Corrosion Attack on a Metal Surface.
Although considerable research has been conducted in this field, many studies are based on simplified or controlled environments that do not fully capture the complexity of real operating conditions. Industrial systems exhibit significant spatial and temporal variability, leading to differences in dominant corrosion mechanisms across components. Addressing this gap requires studies that integrate realworld observations with controlled experimental validation.
The present study adopts this approach by examining three industrial case studies representing distinct chemical environments. The objective is to identify the dominant degradation mechanisms under different conditions and to establish a mechanistic understanding based on post-exposure characterisation of materials and deposits. Alongside this analysis, the study evaluates the performance of thermally sprayed coatings as a mitigation strategy. These coatings offer a flexible and cost-efficient solution for protecting large components, particularly where in situ application is required (Usman et al. 2025). Among the available techniques, arc-sprayed coatings provide a practical balance between performance and deployability. This work therefore investigates the relationship between environmental conditions, degradation behaviour, and coating performance, with the aim of informing the design and selection of protective systems for high-temperature applications.
Industrial Case Studies
Three industrial case studies were selected to examine material degradation under distinct high temperature operating environments. Each case represents a different chemical regime, characterised by variations in deposit composition and gas-phase species, resulting in differences in dominant degradation mechanisms. Material samples were obtained from components exposed to high temperature service conditions. Post-exposure characterisation was carried out to assess both substrate degradation and deposit chemistry. Elemental analysis using scanning electron microscopy coupled with energy-dispersive X-ray spectroscopy (SEM-EDX) enabled identification of key reactive species and their distribution within the deposits and affected material regions.
Case Study 1: Chlorine-Dominated Environment
This environment is characterised by solid-fuel combustion conditions operating at relatively low temperatures (500-600 °C), which favour the condensation and accumulation of highly corrosive molten salt deposits on exposed component surfaces, as shown in Figure 2. Under these conditions, deposited species remain stable in the condensed phase, enabling sustained interaction with the underlying material.
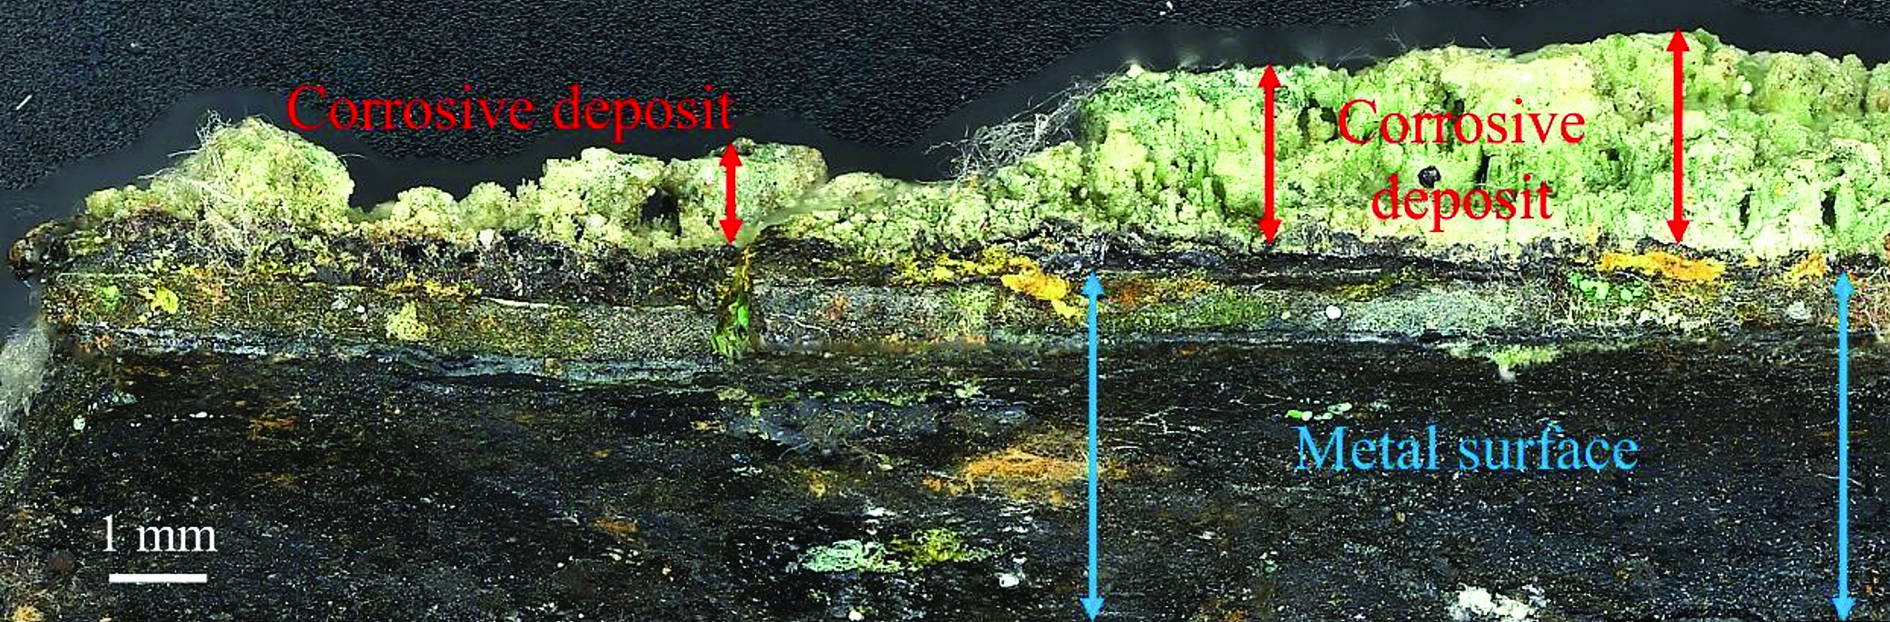
Figure 2: Deposit and Accumulation of Corrosive Deposits on the Exposed Component Surface.
Elemental analysis of surface deposits, as shown in Figure 3, revealed elevated concentrations of chlorine in combination with alkali metals (K, Na), along with iron and oxygen. The presence of alkali chlorides indicates a chemical environment conducive to active oxidation. In this mechanism, chlorine participates in cyclic reactions involving the formation of volatile metal chlorides at the metal-deposit interface. These metal chlorides subsequently migrate outward and re-oxidise in regions of higher oxygen partial pressure, regenerating chlorine species and sustaining the degradation process. This cyclic mechanism disrupts the formation of stable protective oxide layers, leading to accelerated material loss.
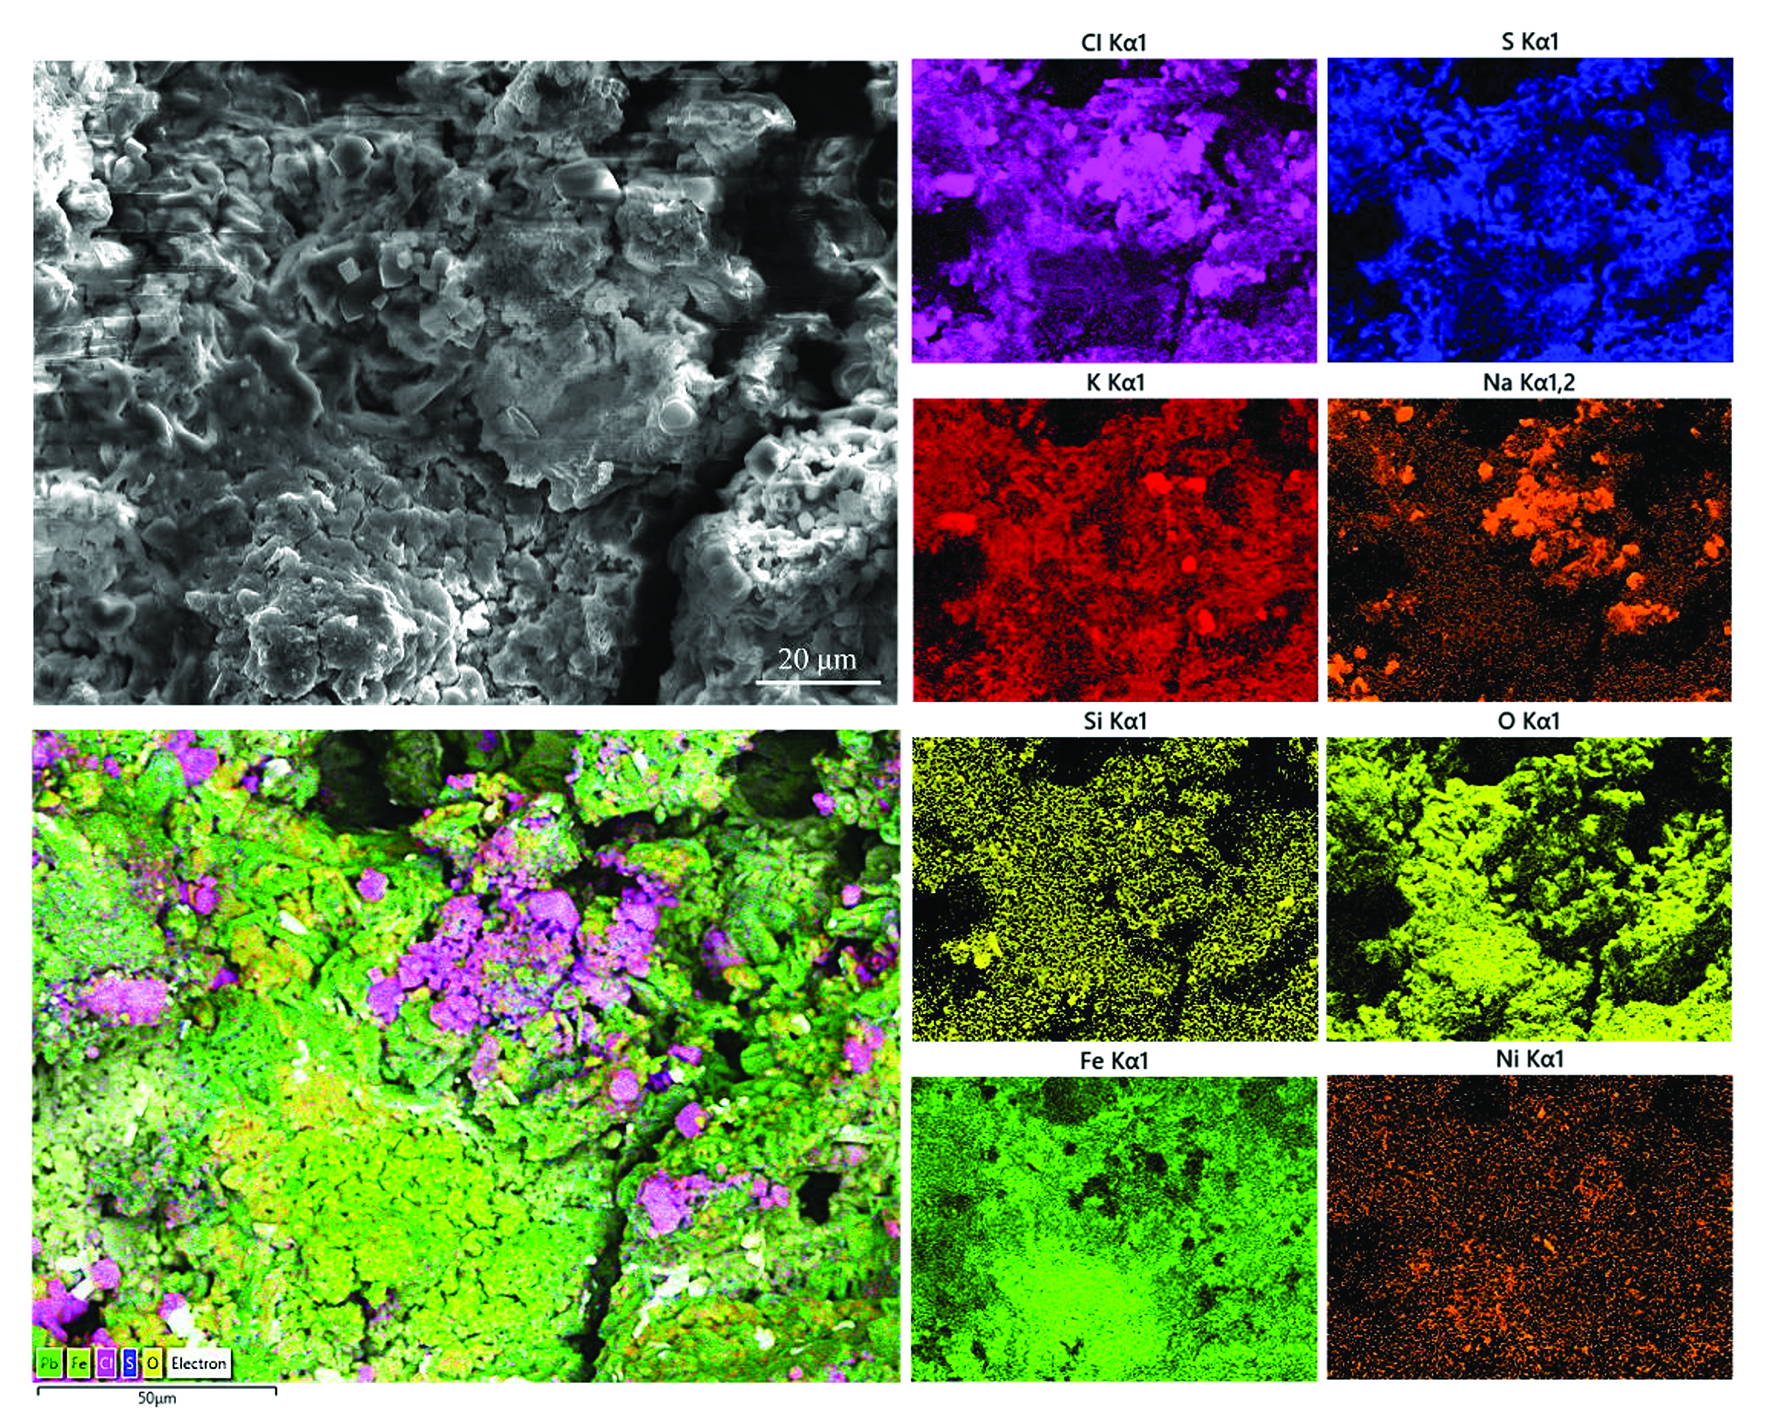
Figure 3: SEM-EDX Elemental Analysis of Surface Deposit from the Exposed Material Showing High Concentrations of Chlorine and Alkali Metals (K, Na).
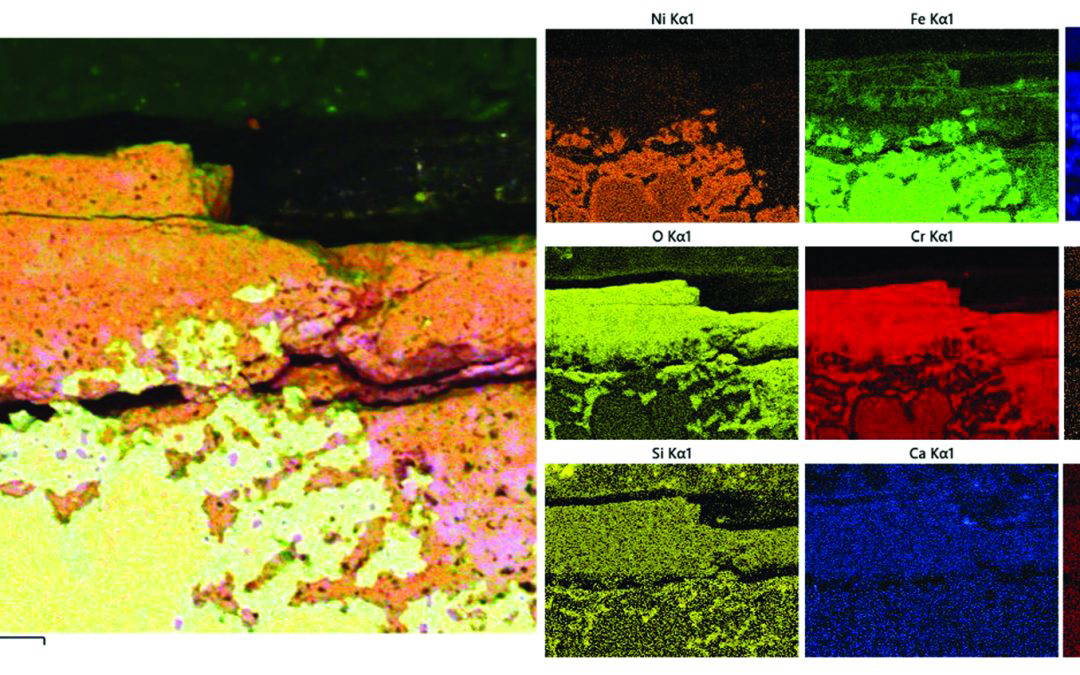
Microstructural observations from the degraded surface (Figure 4) show a porous morphology associated with outward-growing corrosion products. This porous structure is indicative of volatilisation-driven material transport, in which the formation and outward diffusion of metal chlorides result in a non-protective and mechanically weak scale. Elemental distribution maps obtained via EDX analysis (Figure 5) further confirm the localisation of chlorine within these regions, supporting the proposed mechanism of chlorine-driven degradation.
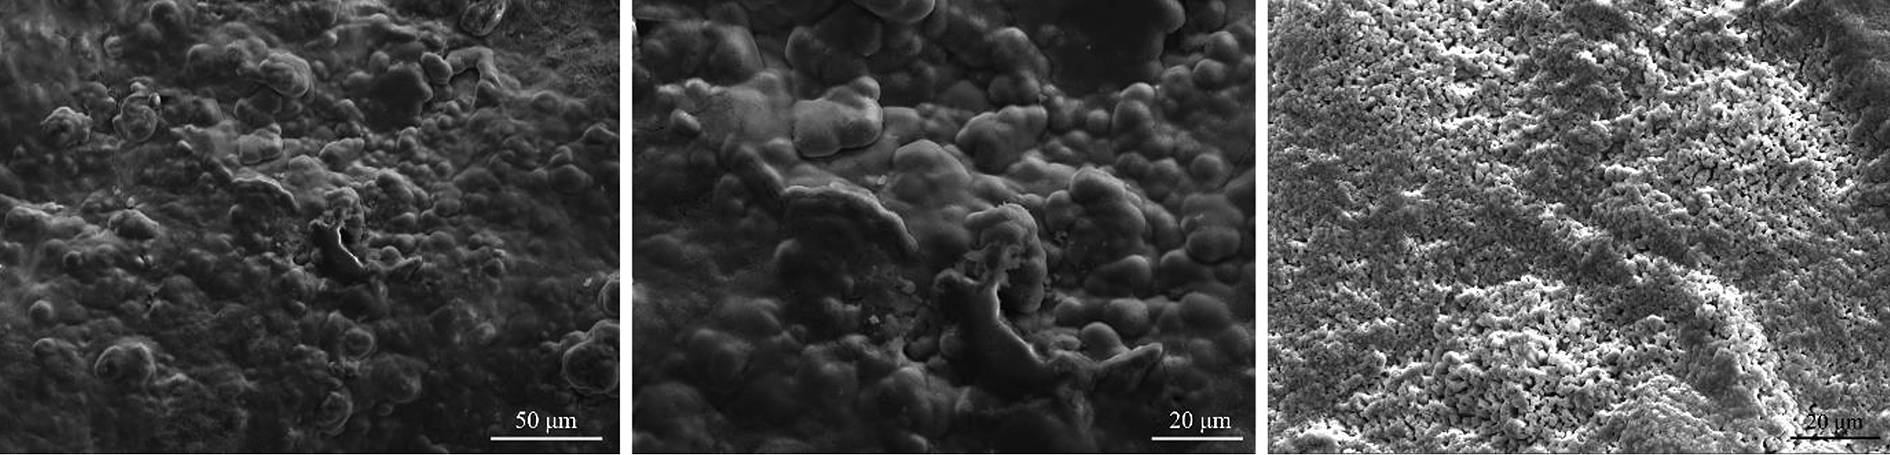
Above: Figure 4: Surface Morphology of Degraded Material Showing a Porous and Outward-Growing Corrosion Product Layer.
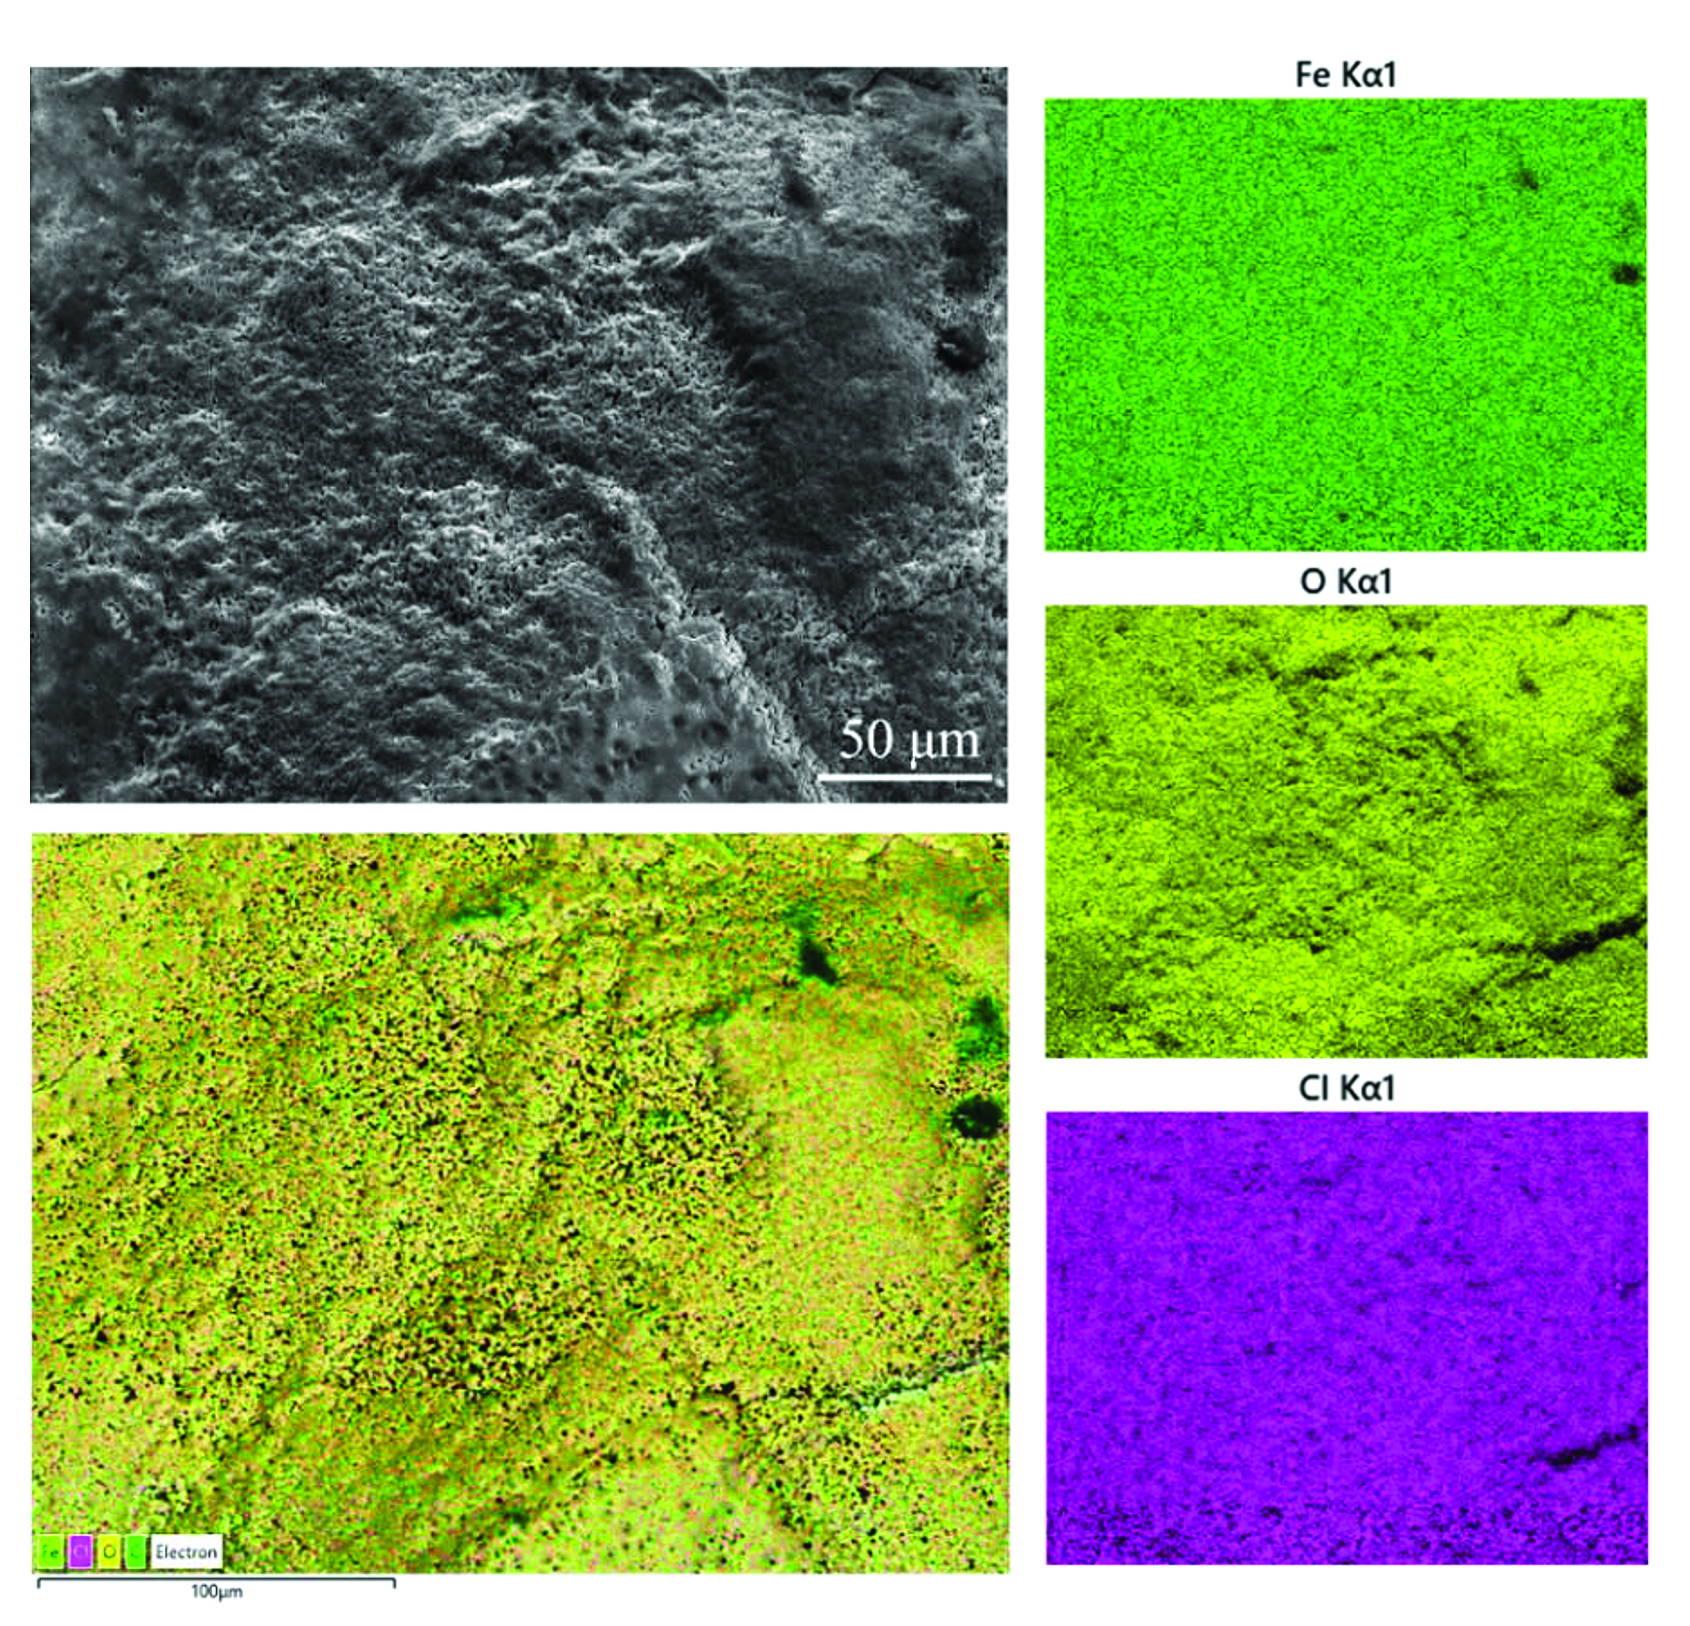
Figure 5: SEM-BSE and EDX Maps of Degraded Region Highlighting the Localisation of Chlorine within the Corrosion Products.
Case Study 2: Sulphur-Dominated Environment
In this study, a 310H stainless-steel component operated at approximately 800 °C under a low oxygen atmosphere with high moisture content. The environment contained sulphur-bearing species, including hydrogen sulphide, carbon disulphide, sulphur dioxide, and sulphur trioxide, along with other process-related compounds. Post-exposure analysis revealed significant sulphur enrichment within the degraded regions, accompanied by redistribution of alloying elements such as chromium, iron and nickel.
Microstructural examination (Figure 6) shows the formation of a layered surface scale, with evidence of cracking and localised breakdown. The outer region is enriched in chromium and oxygen, including the formation of a chromium-rich oxide layer; however, this layer appears discontinuous and mechanically unstable, exhibiting fracture and partial spallation.
Elemental distribution maps (Figure 7) further demonstrate that while chromium and oxygen are predominantly concentrated within the outer oxide layer, sulphur has penetrated beneath this layer into the underlying material.
Within these sulphur-enriched regions, iron and nickel remain present, suggesting the formation of sulphide phases within the substrate. This indicates that the protective oxide layer has been compromised, allowing inward diffusion of sulphur species.
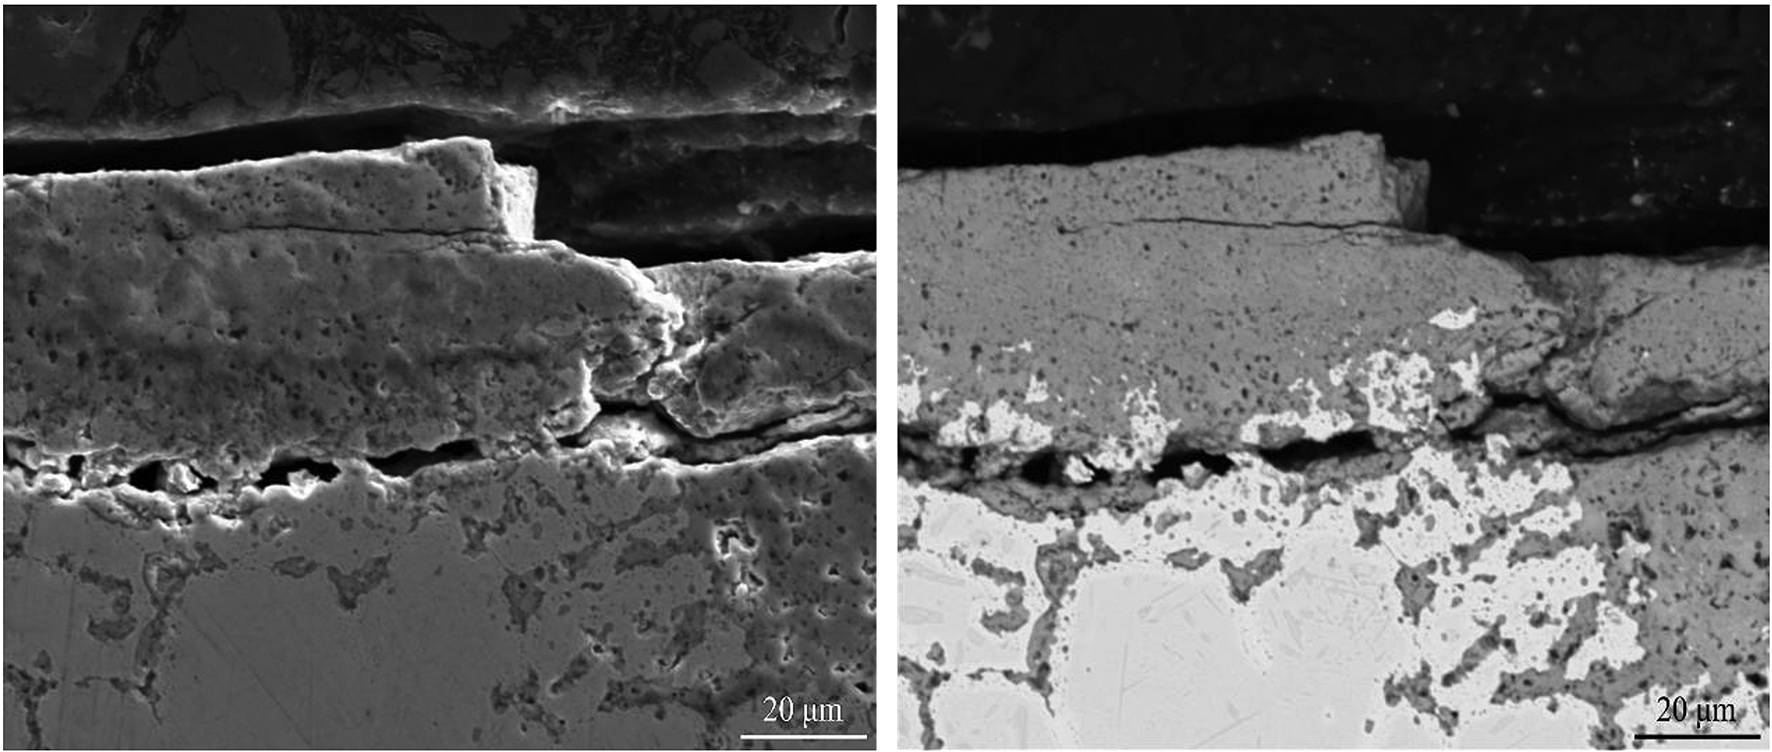
Figure 6: Cross-Sectional SEM Micrograph Showing the Layered Oxide Scale Formed on the Exposed Material.
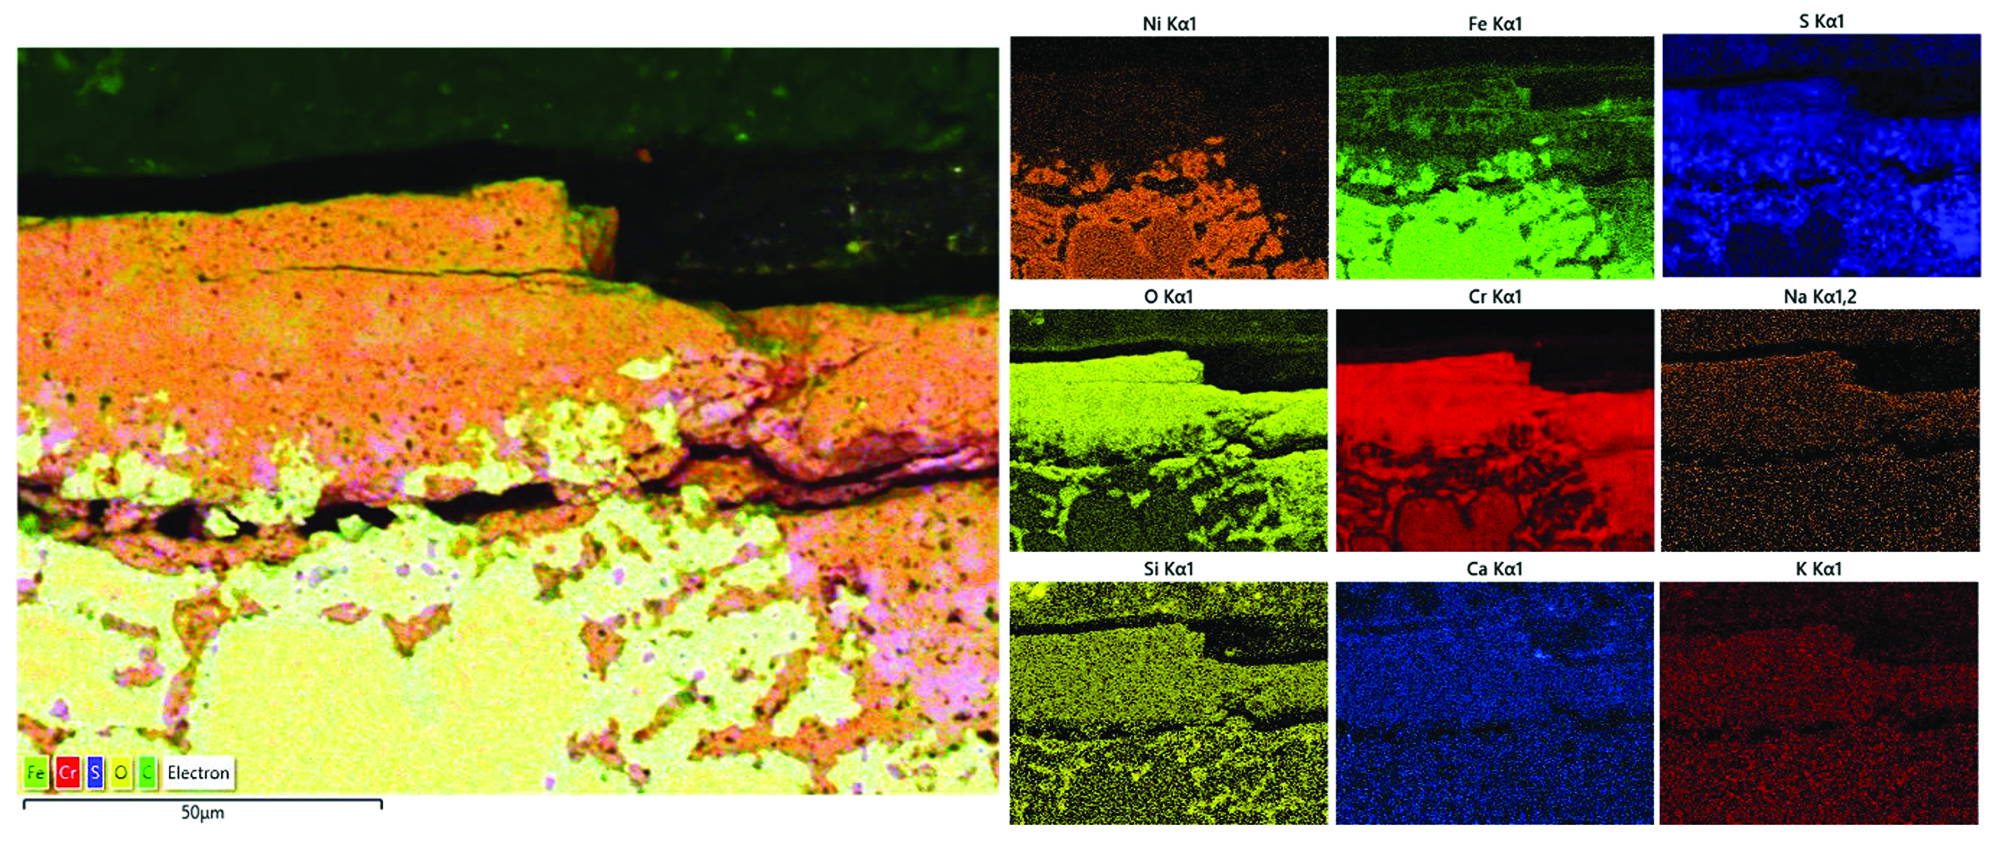
Figure 7: SEM-EDX Maps Illustrating Chromium and Oxygen Enrichment within the Outer Oxide Scale, Alongside Sulphur Penetration into the Underlying Material. The Co-Location of Iron and Nickel within Sulphur-Rich Regions Suggests Internal Sulphide.
Case study 3: Mixed Chemical Environment
This case study exhibited the simultaneous presence of both sulphur and chlorine-containing species, along with alkali metals, indicating a mixed degradation regime.
Such environments are associated with competing and interacting mechanisms, including sulphide formation and chlorine-induced active oxidation, resulting in complex and often accelerated material degradation behaviour.
Elemental maps (Figure 8) from the degraded metal surface indicate the co-presence of chlorine and potassium within the same regions, suggesting the formation of KCl within the deposited salts. In contrast, sulphur is more widely distributed and associated with iron and oxygen.
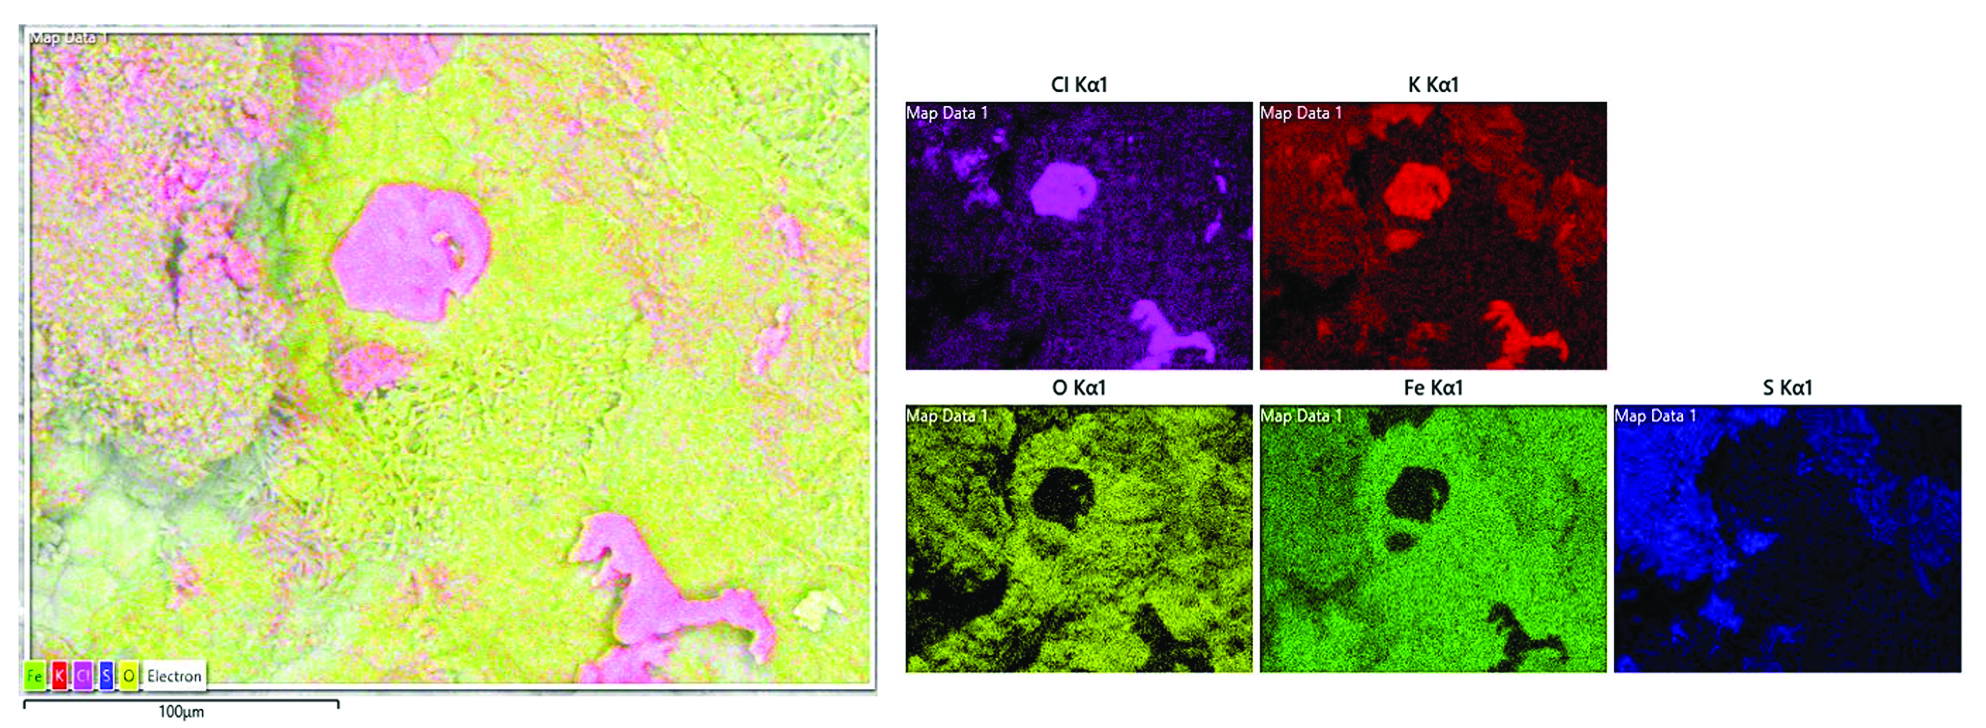
Figure 8: SEM-EDX Maps of the Degraded Surface Showing Co-Localisation of Cl and K, Indicating the Presence of KCl within the Deposits. Sulphur is More Broadly Distributed and Associated with Fe-Rich Regions.
Cross-sectional SEM micrograph (Figure 9) reveals breakdown of the outer oxide scale, accompanied by intergranular attack within the underlying material. The oxide layer appears discontinuous and locally disrupted, reducing its protective capability. Further insight from elemental maps (Figure 10) shows that sulphur, chromium, and potassium are concentrated along the grain boundaries, indicating preferential penetration along these paths. This behaviour suggests that grain boundaries act as fast diffusion pathways, facilitating the ingress of aggressive species and accelerating localised degradation within the material.
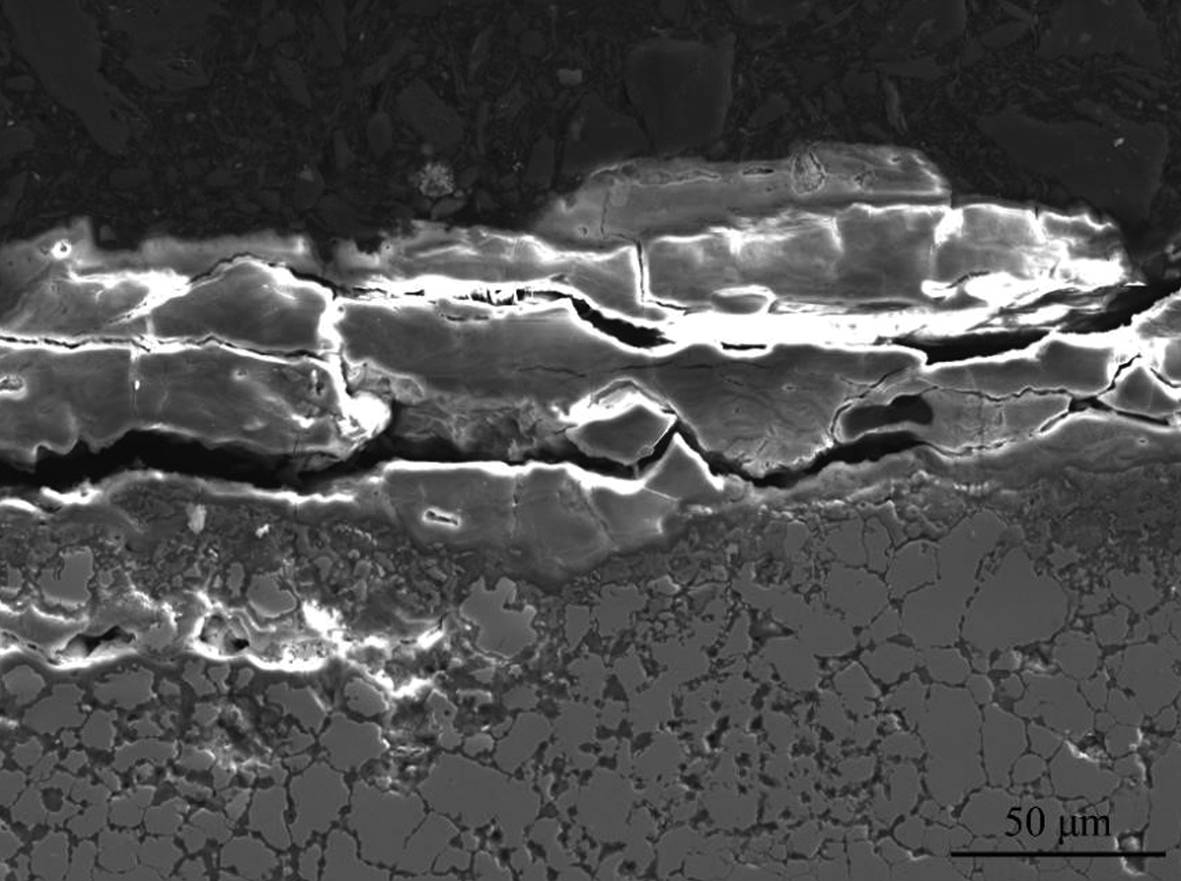
Figure 9: Cross-Sectional SEM Micrograph Showing the Presence of Intergranular Attack within the Underlaying Material.
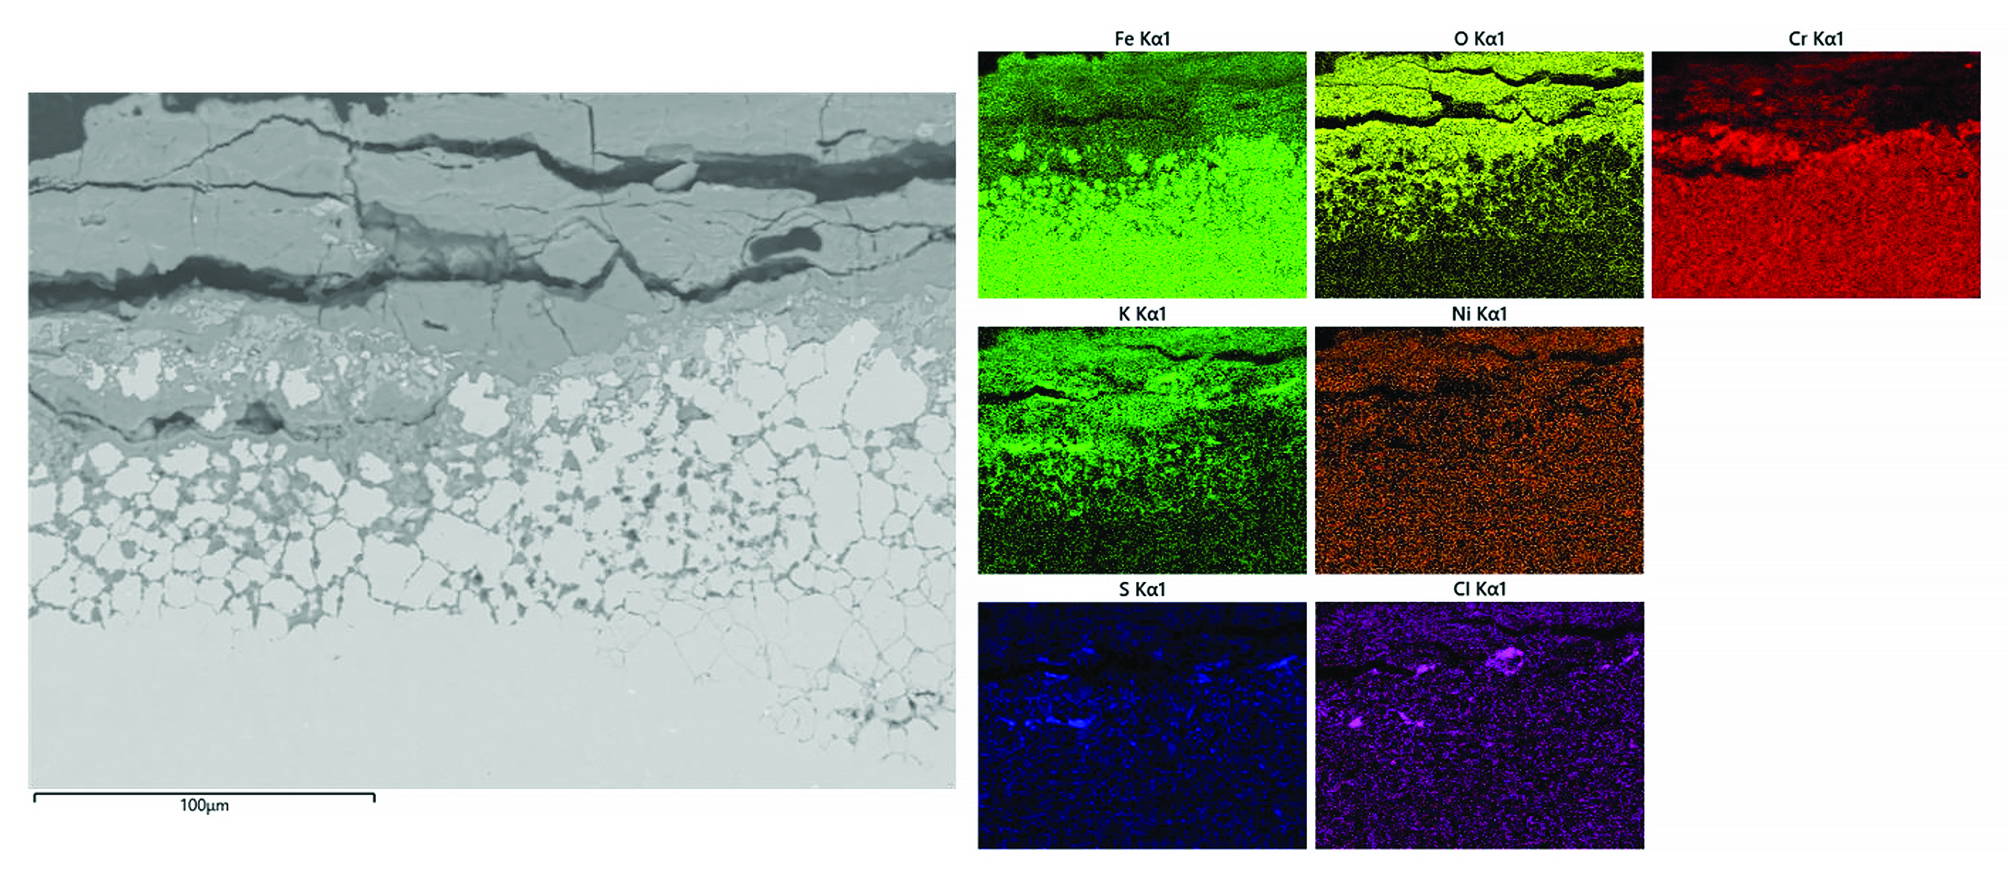
Figure 10: Elemental Distribution Maps Showing the Concentration of Sulphur, Chlorine, and Potassium Along Grain Boundaries, Indicating Preferential Ingress of Reactive Species and Localised Degradation Along These Pathways.
Experimental Procedure and Material
Given the complexity of the three operating conditions identified in the above case studies across different environments, controlled laboratory-scale high-temperature corrosion tests were designed and conducted. This approach was developed to systematically investigate the influence of key variables such as, temperature, exposure time, gas phase composition, and deposit chemistry on the corrosion process.
Arc-Spray Coating
Two cored wire feedstocks were used to deposit coatings via the twin wire arc spraying (TWAS) process (details are reported in a previous study) (Usman et al. 2025). The Ni-based coatings, designated CS-1 and CS-2 (details provided in Table 1), were applied onto 310 H stainless-steel substrate. The coatings were deposited to a thickness of approximately 700 μm.
High-Temperature Corrosion Testing
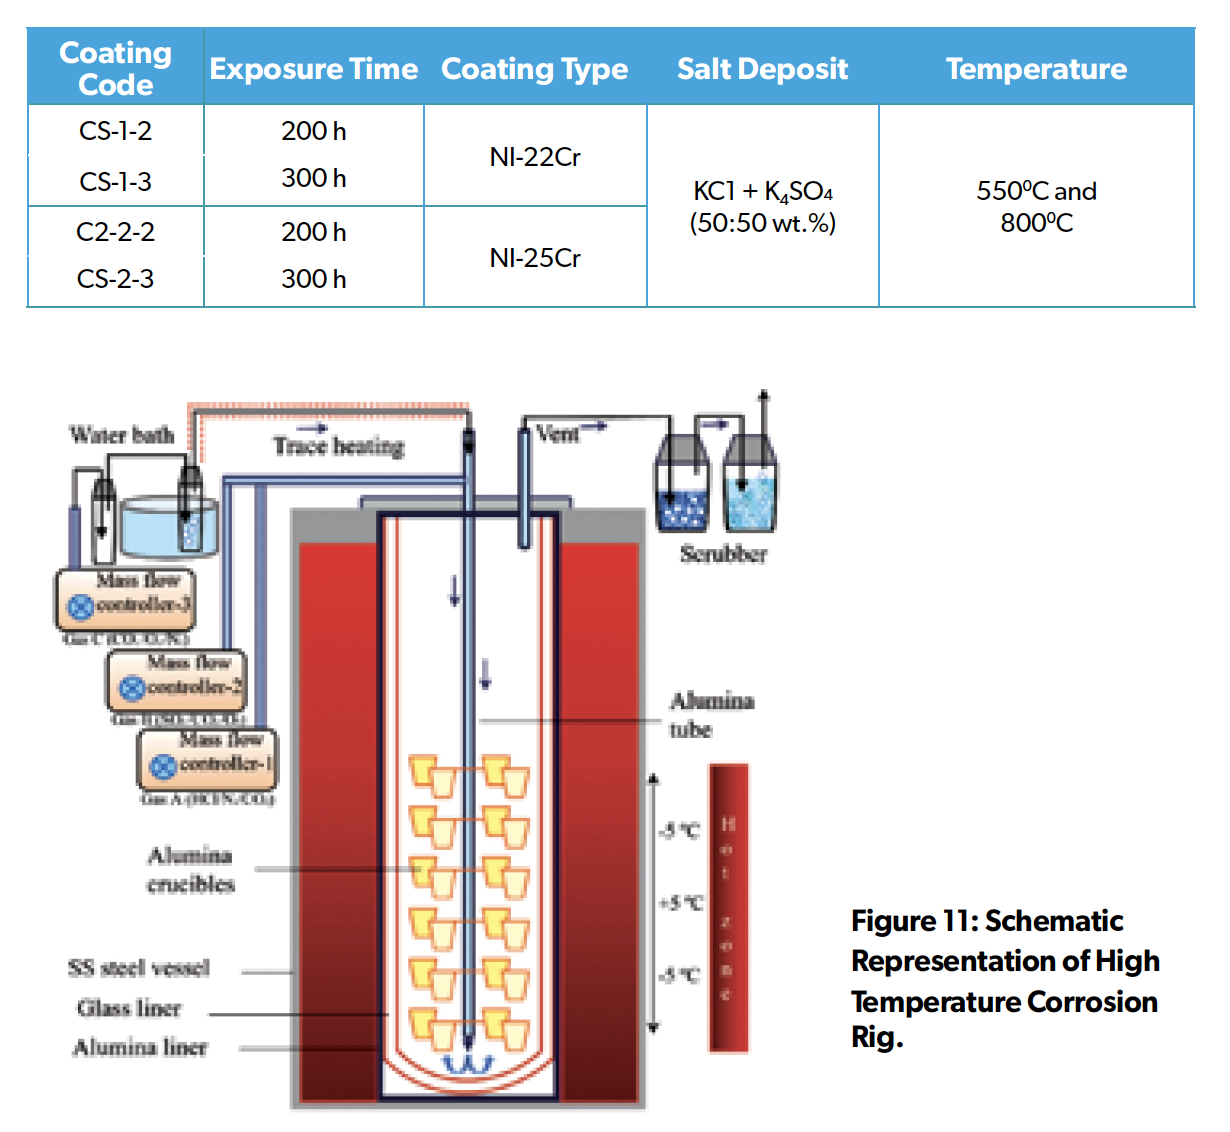
Corrosion tests were conducted under highly aggressive simulated environments containing CO2, SO2, H2O, O2, HCl, and N2 at temperatures of 550 and 800 ± 5 °C, with exposure durations of 200 h and 300 h. A vertically oriented alumina-lined tube furnace (Figure 11) was used to carry out the high temperature corrosion tests under a controlled atmosphere (Waeytens et al. 2023). Coating samples were evaluated under deposited salt conditions comprising KCl and K2SO4. Before testing, coupon samples and crucibles were ultrasonically cleaned in acetone, followed by drying on a hot plate at 100 °C for 1 h before initial weighing. The combined mass of the crucibles, samples, and deposited salts was recorded to determine the applied deposit quantity.
Table 1: Samples Identification Codes and Experimental Conditions.
Post-Exposure Analysis
Following 200 h and 300 h of exposure, coating samples were assessed through cross-sectional microstructural analysis. Samples were sectioned, cold-mounted in low-shrinkage epoxy resin, and prepared using standard metallographic procedures, followed by polishing to a 1 μm diamond finish using an oil-based system. The cross-sectional microstructures were examined using digital microscopy to evaluate coating integrity, thickness variation, and degradation features.
Dimensional Metrology
Coating performance was further quantified using dimensional metrology to assess material loss and degradation (Waeytens et al. 2023). Thickness measurements were obtained along the perimeter of the exposed coatings. Multiple measurements were collected to ensure statistical relevance, and the data were compared with pre-exposure thickness values. These measurements were used to develop probability models describing coating degradation and to estimate coating lifetime under the tested conditions.
Results and Discussion
Microscopy Image Analysis Cross-sectional optical microscopy was performed on all eight coatings following high-temperature corrosion exposure. The micrographs presented in Figure 12 and Figure 13 indicate that all coatings experienced varying degrees of surface degradation. However, the CS-2 coatings exhibited comparatively lower damage than the CS-1 coatings at both temperatures. At 550 °C (200 h and 300 h), the CS-1 coatings showed pronounced localised attack, leading to the formation of a porous and non-adherent oxide scale. At 800 °C, the degradation was significantly more severe, as evidenced by the development of a highly porous surface morphology and coating delamination after 300 h of exposure. In contrast, the CS-2 coatings formed a relatively uniform and more adherent oxide layer at 550 °C, with only limited pitting observed at isolated locations. At 800 °C, although the severity of attack increased, the coatings continued to exhibit protective behaviour, with no significant spallation or deep interfacial corrosion observed.
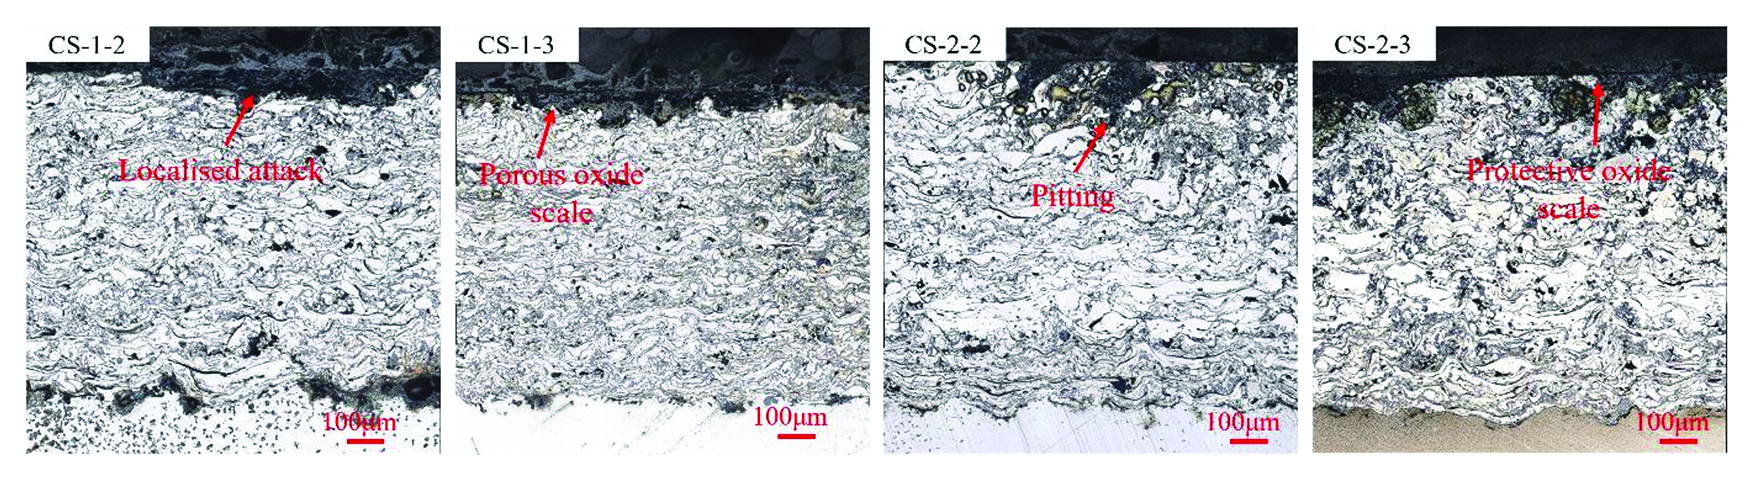
Figure 12: Cross-Sectional Optical Microscopy Images of Samples After Exposure at 550 °C for 200 h (CS-1-2, CS-2-2) and 300 h (CS-1-3, CS-2-3).
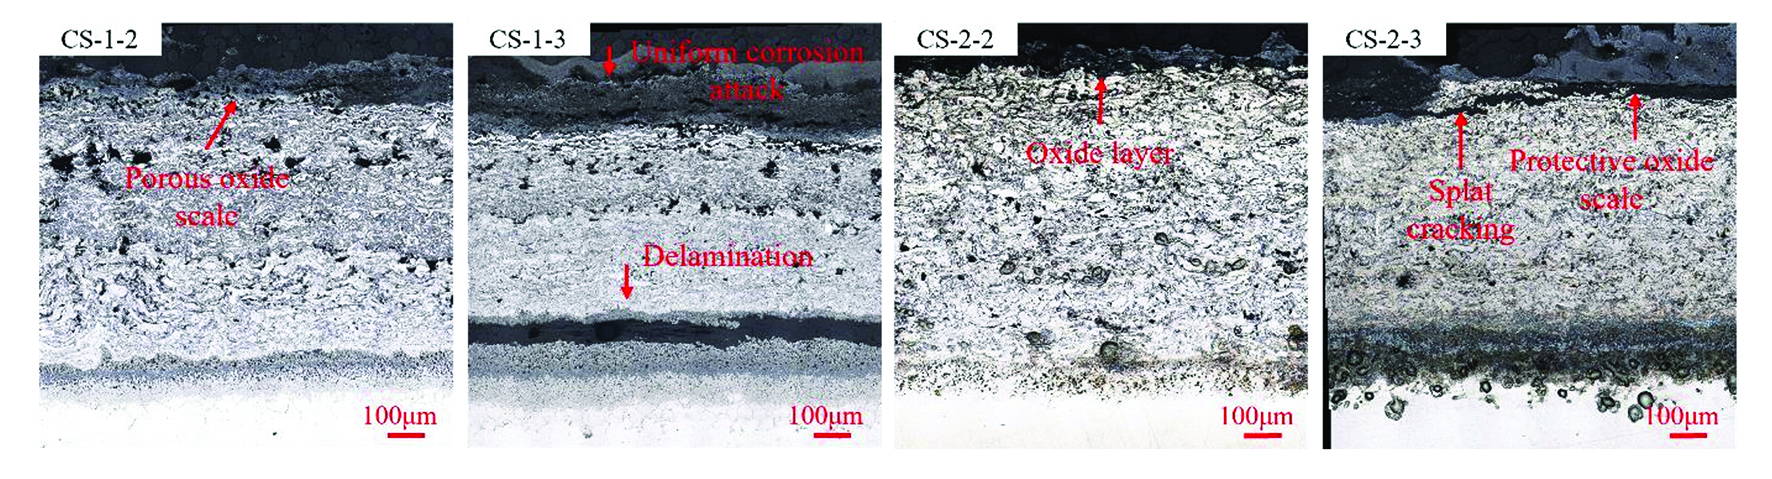
Figure 13: Cross-Sectional Optical Microscopy Images of Samples After Exposure at 800 °C for 200 h (CS-1-2, CS-2-2) and 300 h (CS-1-3, CS-2-3).
Dimensional Metrology
Dimensional metrology analysis was used to evaluate the corrosion performance of coating systems by generating statistical distributions of material loss. The median coating loss values (Figure 14) represent the extent of degradation in the exposed specimens. Figure 14 summarises the corrosion performance of coatings CS-1 and CS-2 exposed to simulated environments at 550 and 800 °C. Across all conditions, CS-2 consistently exhibited lower material loss compared to CS-1, indicating superior resistance to high-temperature degradation. For CS-2-2, the median coating loss was approximately 0.4 mm after 200 h at 550 °C, increasing to 1.0 mm after 300 h. At 800 °C, the corresponding values increased to 0.8 mm and 1.5 mm after 200 h and 300 h, respectively. In contrast, CS-1-2 showed significantly higher degradation, with median coating loss values reaching 5.0 mm after 200 h and 7.9 mm after 300 h at 800 °C.
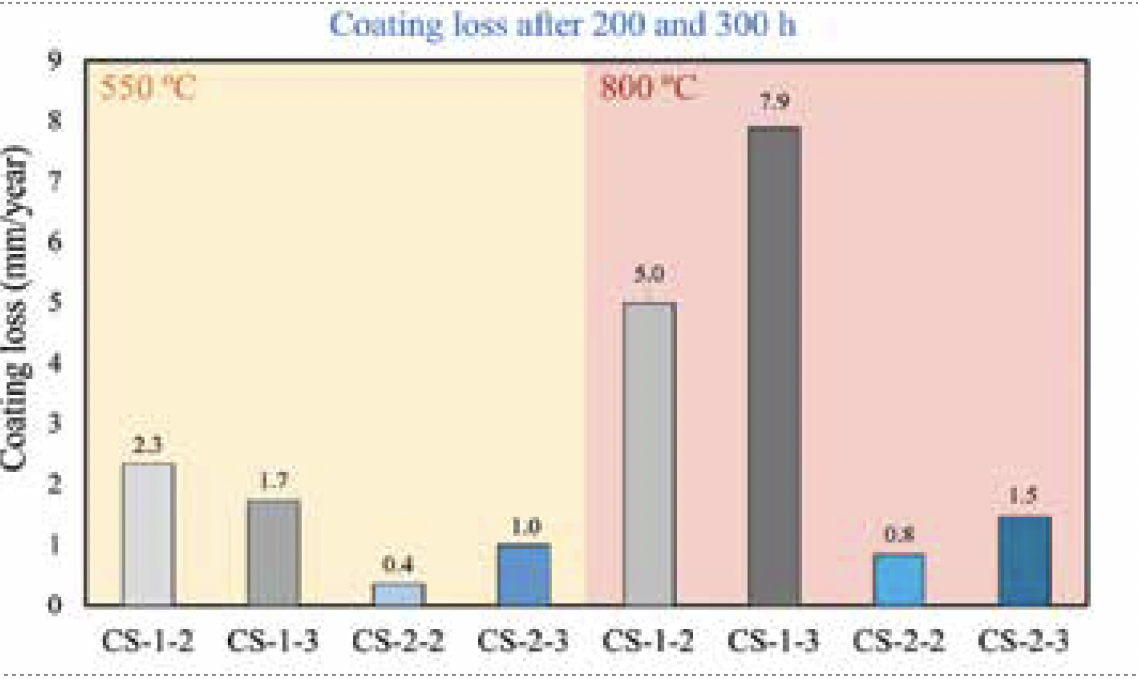
Figure 14: Median Coating Loss of KCl + K2SO4 Deposited Coating Samples Exposed to Aggressive Environments at 550 °C and 800 °C for 200 h and 300 h.
Conclusion
This study investigated high-temperature degradation mechanisms across three industrial environments characterised by chlorine-dominated, sulphur-dominated, and mixed chemical conditions and evaluated the performance of twin-wire arc-sprayed Ni-based coatings under simulated laboratory conditions.
• Chlorine-rich conditions led to the formation of porous, non-protective oxide scales, while sulphur rich environments promoted sulphide formation and internal degradation. Mixed environments resulted in complex attack, including oxide breakdown and intergranular corrosion.
• TWAS coating performance varied significantly between the two systems, with CS-2 consistently outperforming CS-1 under all test conditions. Lifetime modelling confirmed lower material loss for CS-2, demonstrating its superior protective performance at both 550 °C and 800 °C.
• The results highlight the importance of coating composition and microstructure in controlling oxide stability and limiting the ingress of corrosive species. Crucially, a detailed understanding of the underlying degradation mechanisms provides a foundation for the rational design of improved coating materials with enhanced performance in aggressive environments.
Acknowledgements
Special thanks are extended to Dr Adnan Syed, Dr Luis Isern and
Prof John Nicholls from the Centre for Materials at Cranfield University for their technical support in interpreting case study data and corrosion mechanisms, as well as in the development of methodologies enabling coating trials under aggressive conditions. The author also acknowledges Dr Mario Cordero from Welding Alloys Group for his support in the design of new alloy chemistries, which demonstrated good resistance under laboratory conditions, and for his support with arc spray
coating deposition.
References
1. M Spiegel et al, “Fundamental aspects of chlorine induced corrosion in power plants,” Materials at High Temperatures, 2003, 20(2), pp. 153–159. https://doi.org/10.1179/mht.2003.018
2. K Khantisopon et al, “High-temperature corrosion investigations of deposit containing eutectic KCl-K2SO4 mixture on AISI 1015 and SS304 steels,” Corrosion Science, 2022, 205, pp. 110470. https://doi.org/10.1016/j.corsci.2022.110470
3. C orrosion Basics: Understanding the Basic Principles and Causes of Corrosion, Materials Performance, 2011, 50, pp.88.
4. S Floreen and R H Kane, “The sulfidation attack of a nickel-base alloy at intermediate temperatures,” Metallurgical Transactions, 1984, 15A, pp. 5-10.
5. E Sadeghimeresht et al, “Chlorine-induced high temperature corrosion of HVAF-sprayed Ni-based alumina and chromia forming coatings,” Corrosion Science, 2018, 132, pp. 170–184.
https://doi.org/10.1016/j.corsci.2017.12.033
6. A Usman et al, “Fireside corrosion behavior of thermally sprayed coatings for waste-to-energy power plant applications,” Journal of Materials Engineering and Performance, 2025, 34(19), pp. 22393–22405. https://doi.org/10.1007/s11665-025-11630-7
7. M Waeytens et al, “A microscopy study of nickel-based superalloys performance in Type I hot corrosion conditions,” Materials at High Temperatures, 2023, 40(4), pp. 272–282. https://doi.org/10.1080/09603409.2023.2188355