CED Working Day and Symposium on ‘Knowledge Transfer and the Management of Infrastructure Corrosion’
This one-day meeting, held on 27 April at the National Railway Museum, York, is the latest in a series of working days of the CED. There were five main talks after which the meeting broke up into the individual working groups. It was also possible for participants to visit the National Railway Museum.
Nick Smart (Jacobs), Chair of CED, welcomed delegates to the meeting and introduced the speakers. He is stepping down as chairman after 15 years and introduced the new chairman, Danny Burkle. The meeting showed their appreciation for Nick’s excellent efforts during that time and welcomed the new chair.
The first presentation was given by Desmond Makepeace (Galvanizers Association) on ‘Hot dip galvanizing for specification and use in infrastructure projects. Desmond started by describing the galvanising process, and noted the appropriate standard is EN ISO 1461. A variety of defects were discussed. However, it was pointed out that the coating does not have to be perfectly smooth, a certain number of defects can be tolerated, e.g. yellow-orange flux staining, wet storage stains, colour variation, zinc ash, zinc build-up and entrained dross. Other factors affecting the quality of galvanizing were discussed: coating thickness, renovation, adhesion, joining-bolting, duplex systems, maintenance, venting of hollow sections, and overlapping sections. He also discussed how the atmosphere affects corrosion of galvanised structures.
The Young ICorr talk, ‘Best management practices to transfer knowledge to ensure integrity assurance optimisation for oil and gas production’ was given by Izabela Gajewska (Intertek). Knowledge transfer may be defined as, ‘A method of sharing information across different areas in the business’ or ‘A process by which experienced employees share or distribute their knowledge’. In order to address this process, a good plan is needed, which should include work experience, mentoring, training, e-learning, attending conferences, text books, and standards. For best results, a mentor specific to the work situation is required, meeting the ‘student’ weekly or twice monthly, in-person or on-line. The candidate should be furnished with a tailored curriculum and encouraged to give PowerPoint presentations, such as happens with, ‘learn at lunchtime’ talks. External training courses should include subjects such as, basic corrosion, welding, materials, coating, fire protection, cathodic protection, chemical treatments and risk assessments.
Chris Atkins (Mott MacDonald) presented his thoughts on the consequences of climate change on corrosion. He pointed out that historically established corrosion rates in any given environment may no longer be valid, due to the emissions of carbon dioxide that are taking place. The increase in atmospheric carbon dioxide is likely to reduce the pH of natural waters, making them more aggressive to concrete. It will also increase carbonation of concrete, but on the plus side, it may reduce the corrosion rate of galvanized steel. The recognised temperature increase reduces the dissolved oxygen content in water, and Chris showed how an increase in temperature does not automatically produce an increase in corrosion rates. Certainly, any reduction in carbon dioxide levels is likely to reduce atmospheric corrosivity. Chris highlighted that, as far as he is aware, no one is taking an overarching view on the effect of climate change on corrosion, and this could be an opportunity for the Institute to take a leading role.
Richard Barker (Leeds University) addressed the subject of, ‘Academia and industry: How can we advance corrosion science and engineering together?’ It used to be said, ‘academics want to publish and companies want to make money’. However, when research has both scientific and commercial potential, collaboration can be mutually beneficial. Academics have time and research resources and produce new knowledge, and firms are well-placed to commercialise this. However, academia and industry have very different operating environments. Two barriers arise: complexity of communication (knowledge exchange/dissemination) and the complexity of physical collaboration (joint projects). Academic literature tends to be complex, vast and continually changing. To overcome this, industry must trust scientists. Richard pointed out that some companies go to great lengths to identify trusted scientists and research groups. It was concluded that there are significant benefits in collaboration between academia and industry, challenges exist but they can be overcome with the correct approach from both sides.
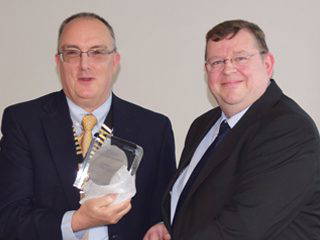
The President then presented the Paul McIntyre Award to Chris Lynch, Engineering Manager at Corrpro Companies, Europe. Chris received the award for his outstanding contribution to a number of aspects of corrosion engineering over a number of years and particularly his work in advancing standards in the area of cathodic protection and supporting the Institute’s training activities (see below).
After lunch, Nick Smart (Jacobs) gave a presentation on, ‘Radioactive waste disposal – where corrosion science meets corrosion engineering’. He elucidated the three main levels of waste. High (HLW), comprising spent fuel/liquid waste which was usually vitrified before being placed in stainless steel containers, Intermediate (ILW), including graphite, waste sludge and structural components, and Low (LLW), of very low radioactivity (e.g. paper, plastics). He described a number of corrosion science research projects that have supported the corrosion engineering and safety assessment aspects of radioactive waste management. Corrosion issues include atmospheric external corrosion of stainless steel waste containers during interim storage, the corrosion behaviour of waste uranium, aluminium and Magnox after encapsulation in cement, and the long-term corrosion of waste containers after disposal in deep geological conditions. The UK total waste inventory has a volume of approximately 4,500,000 m3, which would fill Wembley Stadium! (fortunately, only 0.02% being HLW). The two main concepts for the geological disposal of HLW involve placing copper or carbon steel canisters deep underground and surrounding them with a ‘buffer’ material to prevent release of radionuclides to the biosphere, such as bentonite clay, which swells and provides compressive forces around copper-based containers, or a cementitious buffer material, which provides a highly alkaline environment that reduces the corrosion rate of carbon steel to very low values (<0.01 µm yr-1). Possible geological disposal environments around the world include sedimentary clay, crystalline granite or salt evaporite, with each potential site having different groundwater compositions. Key environmental factors are oxygen concentration, chloride and sulphide concentrations, radiation levels and microbial activity. Nick highlighted the use of a range of analytical techniques to characterise the corrosion behaviour and corrosion rates of candidate waste container materials in long-term in situ experiments conducted under representative conditions. Such studies can be supported by comparison with the corrosion of natural analogues, such as archaeological artefacts, for example the Coppergate Helmet, an 8th century Anglo Saxon helmet made from iron and copper, currently exhibited in the Yorkshire Museum.
This session finished with a short talk by Stuart Bond from AMPP who discussed and highlighted the revised standards development activities carried out by AMPP (a merger between SSPC/NACE was rolled out in January 2021).
The above talks are available in pdf form through the ICorr website in the CED section of the members’ area.
The meeting then split up into the working party section and, apart from the concrete group, all held meetings, short summaries of these follow:
Nuclear Corrosion Group
Following on from Nick Smart’s talk on the interface between corrosion engineering and corrosion science in the context of radioactive waste management, the nuclear corrosion working group, chaired by Nick Smart, held a small meeting which had a wide-ranging discussion about corrosion issues arising during the storage of nuclear waste. These included assessment of pitting corrosion in stainless steel during storage in atmospheric conditions, the effects of microbial corrosion on cast iron under damp conditions, and the potential for galvanic corrosion of stainless steel in contact with graphite in cementitious environments.
Coatings Group
The meeting, chaired by Phillip Watkinson (PW), had seven participants. The minutes of the last meeting in April 2021 were read and approved. The coatings Technical Information Documents (CTID), created in 2016-17, are now due for review. These comprise, Inspection and Testing of Coatings, Surface Preparation Methods, Paint Definition and Generic Organic Coating Types, Thermal Spraying, and On-site and Off-site Application of Intumescent Fire and Corrosion Protective Coatings for Steel Structures. NACE Coatings standards have been transferred to AMPP. G. Maltman pointed out that, as a result of climate change, 15 years standard atmospheric corrosion tests may have to be amended due to changes in RH, rainfall, temperature etc. Douglas Mills (DJM) suggested that EIS measurements (ISO 12944) be reviewed. PW tabled two standards on Paints and Varnishes (BS EN ISO 4628-1: 2003 and 4628-2:2003) also requiring review. Finally, DJM suggested that an interim meeting (possibly via ZOOM) be held ahead of the next annual CED Working Day. This was agreed by the meeting.
Cathodic Protection Group
Chris Lynch was acting chairman of the CP group on the day. In a small meeting, discussion centred on subsea CP systems and performance of flush fit aluminium deep sea anodes on complex piping systems. This included current distribution, current density, anode installation methodology and expected performance along with coatings, anode corrosion products and calcareous deposits.
All Energy Group
This group with Steve Paterson as the chair arose from the Oil and Gas group, with renewable energies now included. This was its first meeting under the new name. Nine people attended. The minutes of the previous Oil and Gas meeting were accepted, although none of the actions had been able to be completed. A good discussion was had (which all those present contributed to) about the purpose of the working group. This covered 1) production of documents (several of the old TACC documents were being revised), 2) Mentoring of young ICorr members, 3) Information exchange via networking, and 4) engagement with other organisations like AMPP. There was also a standards update. It was agreed (as with the coatings group) to try to hold an update Zoom meeting in October.
The delegates.
Nick Smart chaired the closing discussions and thanked the speakers, the Institute of Corrosion, the delegates for attending and the National Railway Museum for providing their excellent facilities. As mentioned at the start Nick is retiring from the CED chair position. And so it is over to Danny, to sort out next year’s meeting. Watch this space!
Report by David Nuttall and Douglas Mills
Personal comments from Nick Smart.
It has been an interesting and rewarding experience for me to be chair of CED for about 15 years. We have held meetings in many venues that I would never have visited otherwise and met many people outside my normal field of work. I am particularly grateful to Douglas Mills, who has helped me in the role. I would also like to thank the working group chairs who have volunteered their time and the many invited speakers (over 60), who have agreed to give a wide range of interesting talks. There is an archive of previous CED talks given in the members’ area of the Institute’s website. A highlight of my term in office was the initiation in 2017 of the Paul McIntyre Award, which is the first Institute award that specifically recognises the achievements of corrosion engineers, rather than corrosion scientists. The CED continues to provide a valuable way of networking between professionals in the corrosion engineering field and of involving up and coming corrosion engineers.
National Railway Museum.
Chris being presented with the award from the President.
The branch March meeting featured a presentation by Dr Robert Lindsay, reader in Corrosion Science and Engineering at the University of Manchester via webinar, entitled “Corrosion inhibition: Separating Fact from Fiction”. Prior to taking up this position in 2005 he had appointments at a number of other research institutions including the Fritz-Haber-Institut (Berlin), Cambridge University, and the CSIC Institute of Materials in Barcelona.
For more than a century, surface-active organic species have been employed to control the corrosion of metals/alloys. Given suitable selection, such corrosion inhibitors have proven to be highly effective, preventing significant degradation of metallic substrates even in highly aggressive environments. Corrosion inhibitors (CI) can be applied in a variety of applications, and most obviously in instances where there are large amounts of aqueous solutions such in the Oil & Gas Industry.
Corrosion inhibitors are substances that, when added in small quantities to a normally corrosive environment e.g. water, gas or oil containing, reduce the corrosion rate (CR) by bringing about a change at or near the surface, without significantly changing the concentration of corrosive species. Layers of corrosion inhibitors can be applied to surfaces to markedly reduce corrosion rate. CI efficiency is measured by comparing corrosion rates with and without the CI coating (film), a CI is considered effective if reduction in CR of >95%, and adequate for corrosion allowance of the material, is achieved.
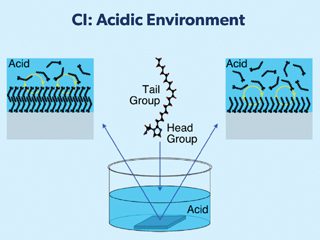
CI can be classed as ‘2D’ or 3D’ adsorbed thin films. The presentation focused on the performance of 2D’ adsorbed films only in low pH, acidic solutions. These frequently have low persistency in operational service (unless CI replenished regularly (at least daily to the system). In an acidic environment of HCl, the main reactions on a steel substrate are the anodic reaction with iron going to its oxide and the cathodic reaction where there is a reduction of protons to form hydrogen molecules. The inhibitor needs to interfere with one or more of these reactions to be defined as an anodic, cathodic or ‘mixed’ type of inhibitor. The inhibitor forming a 2D layer on the surface, shown pictorially as either a monolayer or a bilayer, which is dynamic, forming and re-forming all the time given that there is a balanced supply of inhibitor.
For practical selection in industry, CIs are usually chosen based on users experience by empirical means (historical trial and error), or suppliers’ knowledge and or compatibility with other chemicals already deployed for different production / process reasons. However, to move on, further research is still necessary to fully understand the mechanisms, study of the adsorption thermodynamics (how strongly they bond to surface), and characterise the interfaces, which can possibly lead to ‘green’ CIs being developed.
Understanding how CIs work in detail will allow Industry to move away from an empirical selection process. i.e. are they adsorbing on a clean surface or on top/ combined with salt and oxide, surface?
To this end, current research activity at Manchester focuses on mechanistic understanding of interface properties of relevance to corrosion. Combining electrochemical measurements with surface sensitive probes, such as X-ray photoelectron spectroscopy, to develop structure-performance relationships to enable more complete understanding of corrosion related phenomena.
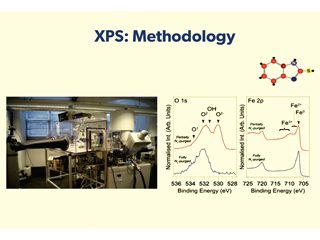
Details of corrosion inhibitor-substrate interactions are being studied through detailed interface characterisation. X-ray photoelectron spectroscopy (XPS), results indicate that the chemistry of the inhibited interface is dependent on both inhibitor concentration and acid identity. The science is highly academic in nature and the physics and chemistry of the studies are best explained by watching the You Tube video presentation at: https://www.youtube.com/watch?v=_-NtzNC7BZo.
Data gathered so far has demonstrated that surface adsorption is not always sufficient for achieving the target corrosion inhibition efficiency, i.e. a surface-active agent can be bound to the surface, but not lead to sufficient reduction in corrosion rate. Moreover, XPS data can be used to argue that the widely adopted approach of determining the standard Gibbs energy of adsorption of a corrosion inhibitor from measured inhibitor efficiencies is flawed, and so should not be relied upon as a tool for corrosion inhibitor selection.
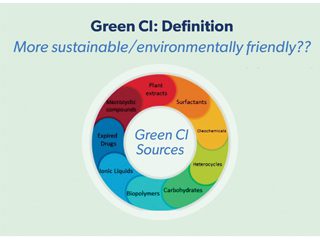
The final message from the presentation focussed on green CIs. We need inhibitors to be more sustainable and environmentally friendly, but a review of the literature shows that little progress has been made and the use of plant-based alternatives (strawberries and other examples) or recycling of waste products (such as coffee grinds) has not received much attention, or is currently judged as having little prospect. However, it should be pointed out that many research programmes have been delayed by the recent pandemic.
In April the branch welcomed Dinko Cudic, Global Technical Authority for StopaqR in a hybrid live presentation/webinar from the Jury’s Inn, Aberdeen entitled “Reducing the environmental footprint for surface preparation and coating application for onshore and offshore assets.”
Dinko is also the technical director for visco-elastic coatings, and has held senior management positions in the Sealed for Life Group who have owned the StopaqR subsidary for more than 15 years.
The energy and utilities industries are now accepting the need to find alternative technologies to reduce waste, CO2 emissions and considerable carbon footprint (product mining/transportation) for steel preparation and coating application. Dinko’s company have developed a solution that addresses, waste reduction, the lowering of CO2, noise and thermal insulation properties, not previously considered in fabric maintenance and asset integrity solutions.
Based on a compound containing non-crystalline, low-viscosity, non-crosslinked (fully amorphous), pure homopolymer polyisobutene, the presentation discussed why such technology should be considered as a viable option, in an industry that requires straightforward maintenance solutions to difficult corrosion problems both onshore and offshore.
Protective coatings are commonly applied to steels, but the integrity of these coatings is dependent on the cleanliness, profile and surface finish of the substrate, and most coatings will simply not adhere or give required lifetime performance unless there is a high-quality preparation giving an angular blast profile and no surface contamination.
In order to achieve this, degreasing compounds are often deployed, followed by abrasive blasting to prepare the new steel substrates or indeed remove old coatings to reapply new ones. The ‘media’ used for blasting is often dependent on the substrate but is essentially hard, angular grit in the form of alumina, garnet, or steel. In the blasting process there are now increasingly demands that all media and the corrosion products, and paint debris, must be safely captured and either recycled or separated and disposed of in a controlled manner, at high cost. However, the environmental cost of mining and manufacturing the media are also quite considerable and with these materials shipped around the world gives rise to a significant carbon footprint. Subsequent clean-up of the paint application equipment means that there are also waste solvents to be recycled and disposed of. Hence the present drivers towards protective coatings that can be applied without extensive surface preparation, or spray application of liquid paints.
Dinko described the target coating engineering requirements, and explained that inspiration for the development of the StopaqR compound was actually taken from chewing gum (!!), an ubiquitous material which adheres to pavements in cities around the world, which is a menace to council authorities. Incredibly, it sticks with no preparation, it flows and adheres, and seals the surface for a lifetime!
In order to develop a product for corrosion protection purposes, polymers available in the open market were studied to look at properties critical to Industry needs, and the product selected that met all criteria was polyisobutene. This product was first developed by BASF in the 1930’s and has a track record in other fields.
In the beginning, solutions were pumped and spread on to surfaces, webbing was added, and a backing or seal coat tape applied for mechanical protection, these were eventually all put into a prepared tape product that could be cut and pressed or wrapped onto surfaces. A particular characteristic of the compound developed was that it remained pliable like a putty, between the surface and the backing tape, so constantly flexible and allowing it to be pressed into all joints and profiles.
The practical application of the product in various fields e.g., buried or submerged piping, splash zone, corrosion under insulation or condensing lines will depend on the international standards and individual company codes that already exist for corrosion protection. Work originally focussed on onshore, above ground pipeline wraps in high salinity, high chloride content environments, desert environments, and then moved on to flanges and awkward junctions where the product was cut to shape and pasted onto the substrate.
The final product can be applied to flat steel in a fashion resembling ‘wallpaper’ using ~ 300mm wide rolls. Essentially the surfaces that it is to be laid onto can first be tested for adhesion by taking a sample and assessing whether it sticks or not.
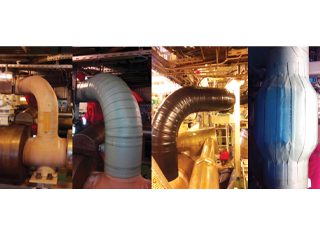
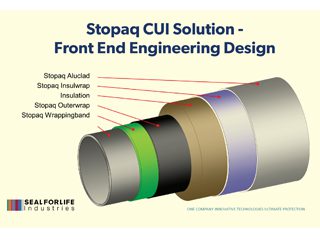
For materials such as stainless steel, surface preparation would remove natural protective films so patches are generally applied directly over natural oxide or flaws. There are also specific system wraps developed with multi-layers to include corrosion protection, insulation, water impermeability, and with outer aluminium cladding.
From the original Oil & Gas industry viewpoint, StopaqR has now moved into applications in civil engineering for bridges and structural supports to offshore renewables – wind turbine towers.
One area in which the product is extremely useful, is in patching damage and sealing small areas by simply cutting patches like plasters from larger sheets and and then applying them.
The presentation also considered the cost advantages of using StopaqR low carbon footprint products. For high quality paint systems 80% of the cost of application is in surface preparation and application but that cost can drop by about 20% for StopaqR type protective compound. The cost over time and the cost to the environment are also significantly reduced along with reduction in risks & HSE associated with the surface prep, materials handling and disposal.
A recent case study of actual cost for the application of North Sea approved epoxy paint systems versus StopaqR for a fabric maintenance area of 550m2 was described. The data from these trials in respect of materials, application and clean up was fully evaluated. Costs for StopaqR system were found to be ~ 2/3 that of a conventional paint system, excluding lifetime costs which can extend maintenance
intervals by 3x.
A comprehensive Q&A took place following both the above presentations which featured significant international attendance.
The branch intends to hold its AGM in September 2022, ahead of the start of the new technical sessions. Abstracts of potential papers for its technical programme are always welcome and these should be sent to:
Hooman Takhtechian, htakhtechian@oceaneering.com
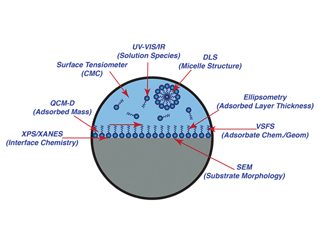
Figure 1 – The Experimental Toolbox
Figure 2 – Summary of Testing Techniques Deployed.
Well summer seems to have started, the weather has improved markedly, the local branches have stopped their technical meetings for the summer, and the North West Branch has organised a golf day again.
This issue features the usual columns, and there is a detailed report on the successful CED working day mentioned by the President. There is a very interesting “Fellow’s Corner” article on the corrosion risks associated with one method of reducing global warming, and both an “Ask the Expert” answer and a technical article look at metallic coatings for corrosion prevention. The other technical article describes a way of mitigating against corrosion of bolted connections.
As always, I welcome comments from readers about the topics covered in the magazine, and how it can be improved. Also remember to send in your technical questions for answer by our panel of experts.
Brian Goldie, Consulting Editor Email: brianpce@aol.com
Welcome to this month’s magazine. We’ve had some wonderful sunshine and that has accompanied a surge in ICorr activity – so I’ll jump straight to it.
In the area of training, I’m extremely grateful to Freyssinet in Telford who continue to allow us to use their facilities for our cathodic protection courses which are in high demand. On the 1st April our conversion course in Portuguese for the Brazilian Corrosion Societies (ABRACO) level 1 coating inspectors to obtain ICorr Level 2 went live, and has already attracted several applicants. We are currently working with ABRACO to translate some of our Industrial Coating Applicator Scheme (ICATS) courses into Portuguese. We are also in discussions with providers for new Refinery Corrosion and Boiler Failure courses.
On the 27th April our annual Corrosion Engineering Division (CED) meeting was held at the National Railway Museum in York with 30 attendees. The meeting was very successful, and it was clear to me that all those present were very pleased to be able to meet in person and resume networking. I had the privilege of awarding our prestigious Paul McIntyre award to Chris Lynch – a very deserving winner from a pool of outstanding applicants.
Congratulations also to Gareth Hinds, our current Past President, who has been elected as the President of the World Corrosion Organisation. I know we’ll here more about this from Gareth in future issues, but he got off to an immediate start in organsing several events for World Corrosion Day on the 24th April. I was honored to be invited to give a virtual talk on the day to the Qatar corrosion community.
On the 16th May I visited the offices of our training delivery partner Corrodere in Farnham, Surrey. Corrodere do a fantastic job of providing our courses in an on-line format, and we discussed how we might expand our current training offer.
It’s been wonderful to see the re-start of activities of our North East Branch who have formed a leadership committee and have several events in planning. A thank you to all involved but especially to David Mobbs for driving this and Lee Wilson for taking on the role of chair.
Finally, and with some sadness I want to let you know that Denise Aldous, our Office Manager, will retire from ICorr at the end of June. Denise has been with ICorr since 2008 and has quietly and enthusiastically built an office that efficiently runs all of our administrative processes. Denise has made an outstanding contribution to ICorr that is impossible to document. Please join me in wishing Denise a long, healthy and fun retirement. At our last Council meeting we presented Denise with a plaque in appreciation of her outstanding service together with a more personal gift.
Have a wonderful summer. Until next time,
Bill Hedges, Institute of Corrosion President Email: president@icorr.org
Ascott have been at the forefront of corrosion and salt spray test cabinets for over 30 years. Their business is totally focused on corrosion test equipment, and today they are one of the leading suppliers of salt spray cabinets and cyclic corrosion cabinets in the world, exporting to over 45 countries.
Everything produced is manufactured in their factory here in the Midlands, with local suppliers very much at the heart of the supply chain. Their latest range embodies customer led innovation, blending performance and technical excellence. The creation and control of corrosive climates has never been more demanding, and the development of new materials and surface coatings, plus increasing user expectations, has given rise to ever more rigorous testing. This is their forte.
Their expertise is the reassurance that a customer needs to ensure their testing is precise, compliant, and repeatable. Their equipment leads the world technically, but they also pride themselves on offering excellent value for money. Investment in an Ascott chamber offers the customer consistency, reliability, and, with their premium level of after sales support as standard, a high degree of confidence.
Many test standards can be complex and difficult to interpret, and the customers rely on their expertise, experience, and knowledge in this field to guide them to the exact product that will meet their needs. Every chamber is built to individual customer specification, even down to incorporating customer branding and corporate colours if required.
They also supply a comprehensive range of laboratory and field test equipment and consumables via an online shop, offering a convenient and trusted one stop solution for all your testing requirements.
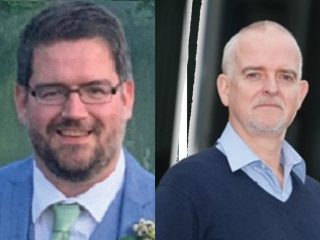
The January technical meeting featured a presentation by Joshua Owen (pictured left), Research Fellow in the Institute of Functional Surfaces, School of Mechanical Engineering, University of Leeds, on “Advanced once-through flow cell methodology for validation of a new ‘staged’ inhibition approach for matrix acidising treatments” as part of a collaboration between Schlumberger and Leeds to evaluate staged inhibitor approaches prior to industrial application.
Schlumberger recently introduced and patented a new staged acid corrosion inhibitor (ACI) treatment concept for application in matrix acidising treatments. The staged treatment concept recognises that treatments which employ a fixed dosage of corrosion inhibitor may not be optimal in terms of their efficiency. The concept proposes staged pumping of a first fluid composition designed to establish a persistent inhibitor film (Stage 1) and a second fluid composition to maintain the film and its associated inhibited corrosion rate (Stage 2). The staged ACI concept has the potential to provide enhanced corrosion protection of wellbore casing and coiled tubing (CT) materials, whilst using the same total quantity of inhibitor compared to conventional treatments.
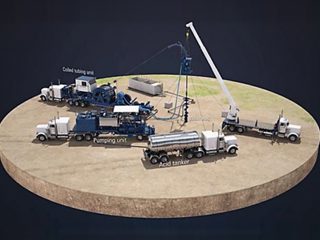
Typical Onshore Well Acidising Treatment.
Typically, the corrosion test methods used to evaluate this approach have involved preparing two equivalent pre-heated and conditioned glass reactors, one of which is used for the first film-forming stage and the other for the second film maintenance stage. This procedure is rather inconvenient and involves a short period of time (~1 min) during which the weight loss coupons or working electrode (a rotating cylinder electrode) are in contact with the atmosphere which could change the corrosion potential and could potentially have an influence on the inhibitor film formed during the first stage. Instead, a bespoke, electrochemical, milli-fluidic once-through flow cell was used for validation of the staged ACI concept by exposing a carbon steel coupon, mounted within the flow cell, to 4 M hydrochloric acid (HCl) flow at a temperature of 80 °C and a flow rate of 5 ml/min. A once-through flow cell enables testing in a continuously flowing environment whilst maintaining a fresh acid solution, a controllable supply of inhibitor, and eliminating any contact of the electrode with the atmosphere.
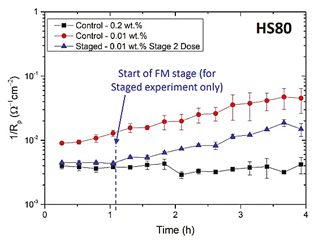
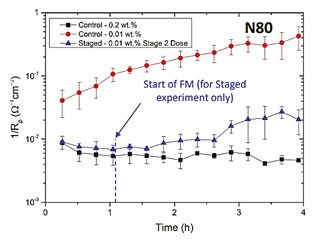
The system was used to quantify changes in corrosion behaviour during continuous flow and during transitions from the first to second stage inhibitor dosages, to find optimal inhibitor concentration for film-forming and film maintenance stages, and to investigate the effect of metal pre-corrosion on inhibitor performance for carbon steel used as wellbore casing and CT materials. In situ linear polarisation resistance measurements confirmed that an acetylenic alcohol-based polymerisable inhibitor, used at a concentration of 0.01 wt.% in Stage 2 after a 0.2 wt.% concentration film forming stage (Stage 1), maintained excellent corrosion protection of N80 (wellbore casing) and HS80 (CT) carbon steel, with corrosion rates of < 5 mm/year measured.
Significant corrosion rate reductions achieved with staged inhibition versus applied controls.
Advantages of the flow cell for application in ACI studies are:
1. Well-defined hydrodynamics: Consistent and predictable flow across metal surface once-through nature:
2. Fresh HCl and ACI are continuously replenished and flow into waste, maintaining consistency in experimental conditions throughout In situ electrochemical measurements:
3. Measurements of corrosion rate in real time seamless condition changes:
4. Composition of fluid can be easily changed prior to inflow during an experiment (no exposure of coupon to air)
For the February presentation, Leo Richards, Principal Engineer and Andrew Duncan, Lead Consultant, both with Intertek Production and Integrity Assurance Group, described the “Implementation of Plan-Do-Check-Act review.
Leo Richards (left) Intertek Principal Engineer Production Chemistry and Andrew Duncan (right) Intertek Lead Consultant, Production and Integrity Assurance.
Corrosion management guidelines were used as the basis for an audit study of a large onshore oil field, the purpose of which was to perform a detailed review of the corrosion monitoring and mitigation systems, and to advise on any required upgrades to ensure world class/excellent asset integrity performance.
The approach taken for the study was to follow the UK Health and Safety Executive’s guidance for ‘Managing Health and Safety’, HSG65 (2013), of PLAN-DO-CHECK-ACT, which considers both Technical and Systems approaches associated with managing assets safely. This is a closed loop planetary model commencing with a high-level corporate policy for health and safety, under which there is a policy and plan for managing corrosion and integrity. The model ends with lessons learned which feed back into the corrosion and integrity policy and plan to ensure risks are managed to ‘As Low as Reasonably Practicable’.
The model ends with lessons learned which feed back into the corrosion and integrity policy and plan to ensure risks are managed to ‘As Low as Reasonably Practicable’.
First, a detailed study was carried out to assess and identify the current corrosion management techniques being used and their effectiveness in the operator’s fields and process plants. The ‘gaps’ were identified within the assets, and corrosion management proposals and solutions were then provided to ensure world class asset integrity performance.
A desktop-based document review was conducted in the UK and also at the client’s offices. This was followed up by site surveys, which included visits to at least one plant of each of these facility types: gas station, degassing station, gas recycle plant, PWI stations, gas distribution stations and stripping plants.
In order to help delegate and spread some of the responsibilities for the study areas within the operator’s corrosion team, Intertek deployed RACI Charts: Responsible – Accountable – Consulted – Informed, which serves to provide structure to the corrosion team as a whole, defining who does which task and allowing the right people to do the right job and move on with it.
The study highlighted a distinct pattern in the working practices of the operator with virtually all sections of the corrosion management system being shown to have some form of PLAN and DO. However, the implementation of the CHECK and ACT stage was missing from almost all aspects.
Some Key Findings
1. Automation and use of a suitable database/Corrosion Management System makes the DO stage easier and quicker.
2. For CHECK and ACT – an automated system requires Specialist assessment, rather than total reliance on the CMS output. Automation may also result in complacency.
3. For CP monitoring, sensors need to be regularly calibrated, and the system checked to ensure full protection.
4. Data requires to be both CHECKED and reviewed.
5. ACT will have double impact – ACT on what the data has shown and ACT on how the data was gathered.
Future Application of P-D-C-A and Corrosion Monitoring
The working world has changed dramatically over the last two years due to Covid and there has been a significant change in Engineers’ working patterns and methods of project study and delivery. This has also combined with a move towards remote and automated inspection and monitoring, however, the speakers were keen to stress that if the PLANNING Stage is not implemented correctly, then wholesale automation of integrity systems is not always helpful, as automated systems will follow ‘Garbage In Garbage Out’ scenarios, Specialist input is always required. (Editor: Readers should note that a longer technical article on this topic appears later in this issue of the magazine).
Both these very engaging presentations generated many questions from the audience that were expertly responded to by the speakers, and all Q&A write-ups may be found on the branch webpage.
Slides of technical papers for branch events, along with their respective Q&A’s can be found at, ICorr Aberdeen Branch (google.com) under Local Technical Programme, Aberdeen Branch – Institute of Corrosion (icorr.org). A library of event recordings may also be found at: ICorr Aberdeen – YouTube.
It is also with our great pleasure to announce that Rysco International Inc. based in Alberta, Canada, has become the latest new sponsor of the branch, as well as becoming a GOLD sustaining member of ICorr. The branch is very grateful to all its sponsors for their continued support.
Finally, the branch is very sad to report the recent passing of Carol Anne Powell BSc., FIMMM, a long-term consultant to both the Nickel Development Institute and the Copper Development Association.
She had written over 40 papers and publications and been a member of our Partner Organisation the Marine Corrosion Forum (MCF), since its inception. During the recent COVID-19 epidemic as we were moving increasingly towards Webinar formats in April 2020, Carol greatly assisted us with an excellent presentation to our ICorr/MCF membership entitled ‘An Overview of the Corrosion of Metals in Seawater. In her memory, we would respectfully direct you to: https://marinecorrosionforum.co.uk/free-webinar-30%2F04%2F2020
The Aberdeen branch would like to invite you (or a colleague) to give a presentation during their 2022/2023 session. The events normally are held at 6 pm on the last Tuesday of the month from September till May 2023, excluding December 2022.
Topics on pressure systems, pipelines, renewables and structural integrity management with regards to the material selection, production chemistry, welding, corrosion/microbiological control and monitoring, inspection techniques and data analytics, are acceptable. Past case studies, project experiences, and emerging technologies have proved popular and interesting to members, and are particularly welcome.
The attendees (members and non-members) include students, technicians, technologists, engineers, scientists, researchers, managers, company directors and other professionals from the oil and gas, power generation, manufacturing and renewables sectors. Subsequently we would publish a report of the presentation in Corrosion Management magazine, and also on the ICorr, and Aberdeen website pages, including the presentation slides and Q&A session write-up. A recording of the event (if conducted online) will be uploaded to our YouTube channel later.
If interested, please supply the following including, speaker’s name, role and company, short biography of the speaker(s) (~ 150 words) and the proposed presentation title and an abstract (400 words), to the ICorr Aberdeen Branch Chair, Hooman Takhtechian, via htakhtechian@oceaneering.com and please also copy in icorrabz@gmail.com in your submission.
All the submitted presentations will be subject to a branch committee review and those successful will be scheduled into the 2022/2023 events programme. Please note that the deadline of the submission is
30th April, and the branch will confirm the successful presenters in May, and announce them in June.
We use cookies to optimize our website and our service.
Functional
Always active
The technical storage or access is strictly necessary for the legitimate purpose of enabling the use of a specific service explicitly requested by the subscriber or user, or for the sole purpose of carrying out the transmission of a communication over an electronic communications network.
Preferences
The technical storage or access is necessary for the legitimate purpose of storing preferences that are not requested by the subscriber or user.
Statistics
The technical storage or access that is used exclusively for statistical purposes.The technical storage or access that is used exclusively for anonymous statistical purposes. Without a subpoena, voluntary compliance on the part of your Internet Service Provider, or additional records from a third party, information stored or retrieved for this purpose alone cannot usually be used to identify you.
Marketing
The technical storage or access is required to create user profiles to send advertising, or to track the user on a website or across several websites for similar marketing purposes.